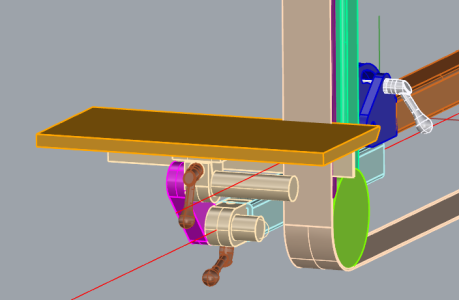
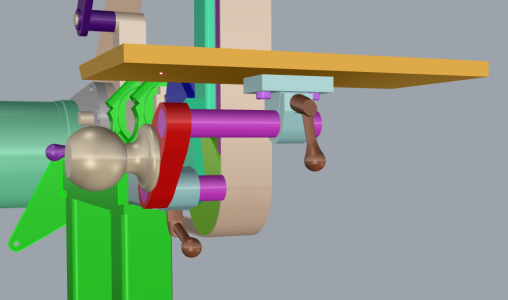
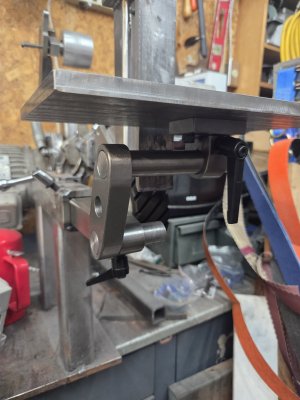
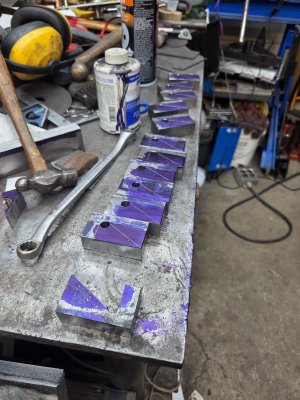
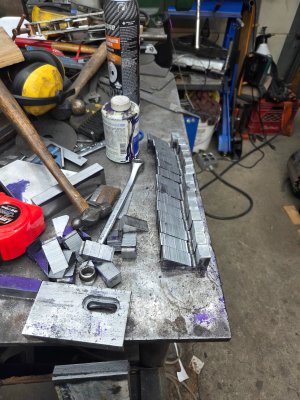
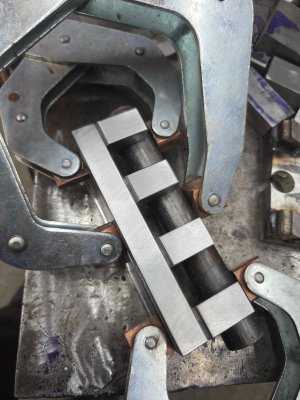
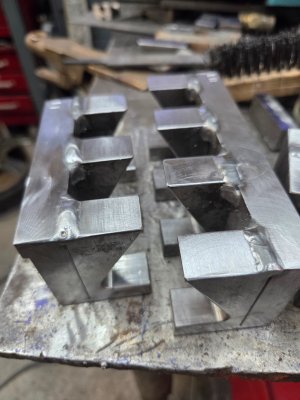
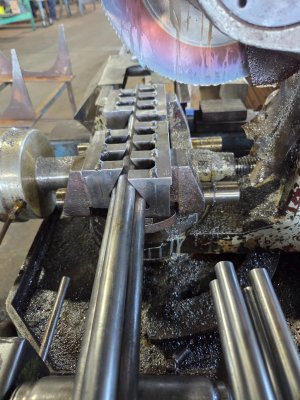
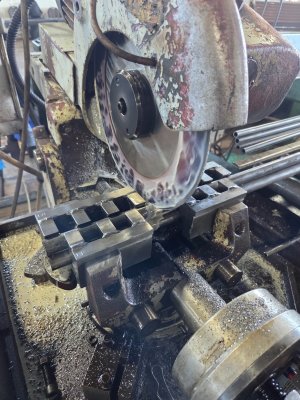
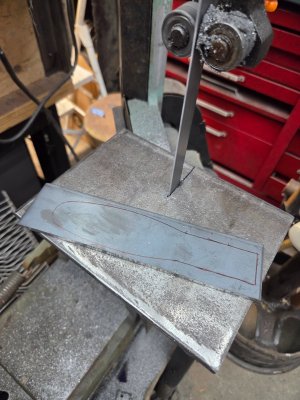
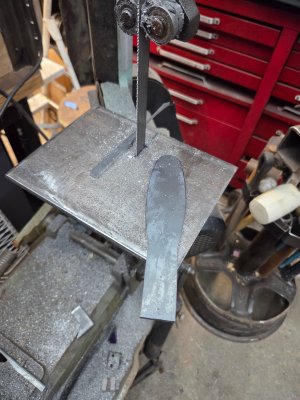
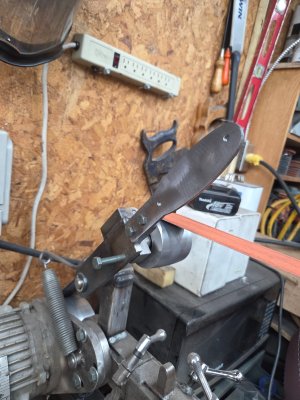
Well, today didn't quite pan out like I was hoping, twas a day of many distractions, but I still managed to find enough stock and adjust the model to fit what I ACTUALLY had (7/8" shaft vs 1" designed, and adjust some block sizes....), then start squaring up and machining things. Not done, perhaps a few more hours tomorrow, but by end of day, I should have an adjustable table and a fully functional grinder (sans extra attachments of course). Then I'll probably actually do a complete build thread on it, instead of just snippets in this one....
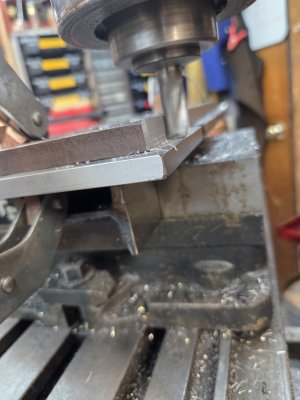
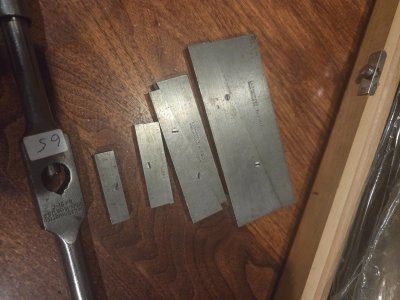
Drilled the clamp screw holes at a 15* angle. A long time ago I read about using a ball endmill for spotting holes on angled or curved surfaces. I'll admit, I've never had to do much of it, maybe a dozen times or so, but when I need to, that's been one of those tips that works really well and is worth knowing. Spotted with a 3/8" 4fl ball, drilled 17/64" (M8), spotfaced with 3/4" endmill, then walked it out the end for a flat bottom, and finally drilled for clearance to a 0.3" depth. All Located with a pointed wobbler from scribe lines, and done for both blocks. I used a 15* angle block in the vise to set the angle.
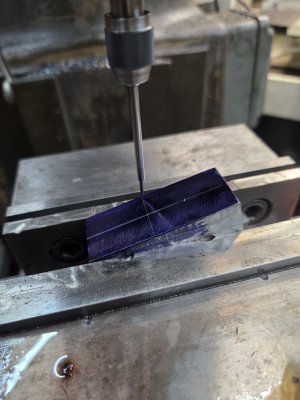
Should have went deeper with the spot here, this one walked a bit on me. Not bad, but enough for me to notice....I corrected it on the bigger block, and it was fine.
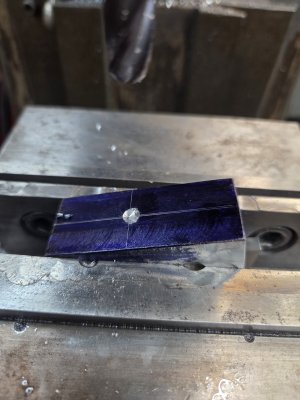
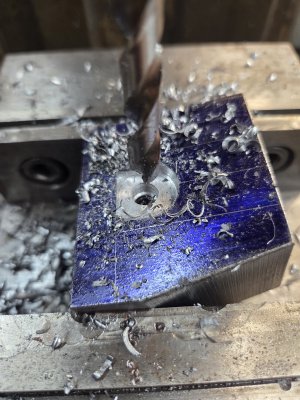
Tapped m8 with my recently made tap wrench.
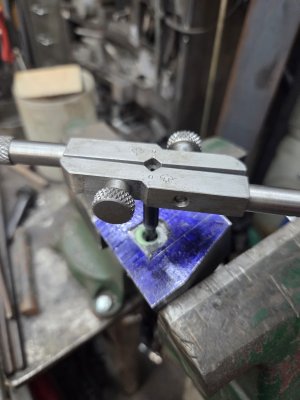
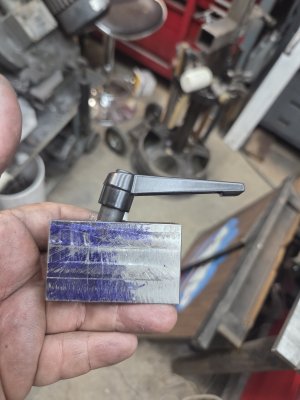
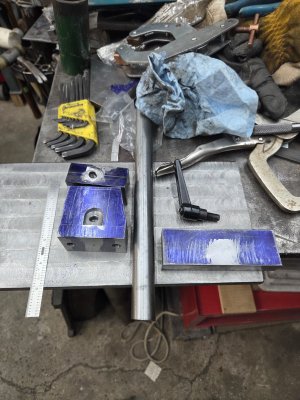
The rest should be pretty straightforward tomorrow. I'll be using the Tormach to round the ends but really wish I had a rotary table though.....Still undecided on how I'm going to do the bores. 2 slide fits, 2 press fits on the link. Leaning towards manually boring them, but will probably interpolate and save a setup.