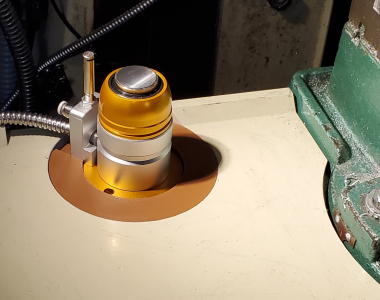
Well now. The new tool setter just arrived.
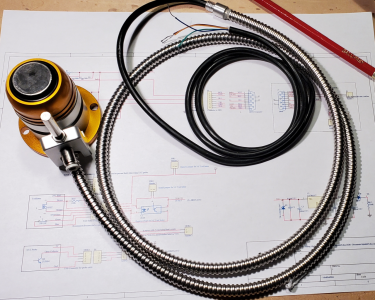
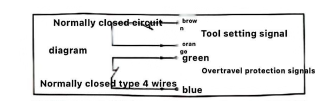
It's a Normally Closed version (NC) rather than Normally Open (NO) like the previous one I smashed and bent. To make the NO one work I had to add a small circuit that changed the polarity of the signal before it went into the probe input pin.
Both these tool setters also have a NC mechanical over travel switch. NC so that if the wire or connector breaks it stops the machine. This is assuming of course that's even wired into the system. And there's the rub...
The spindle encoder, tool setter and probe circuit board in a small box up by the spindle motor and pulleys has a connector on it that is supposed to take the two wires from the over travel switch down to the limit switch box that collects all the limits. The plan was to have the tool sensor in series with the limit switch so that if it were actuated the effect would be the same as the ESTOP all would stop NOW!
Well the limit switch interface box also has a two pin connector in it and a jumper sitting on it faking out the closed tool sensor over travel switch.
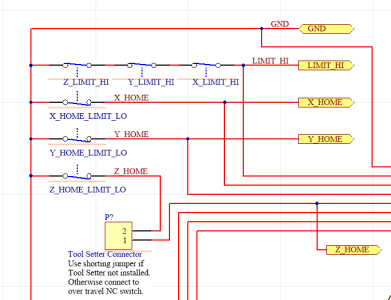
Oops. For some reason I never took the next step and added the two conductor wire and two connectors so that the signal from one was brought to the other. I do have a new cable there now...
And speaking of cables. The armoured part of the new tool setter is half the length of the other one and thinner because it has only 4 wires. Also the cable inside that extends out only 1/4 as far as the original. So it won't reach anymore. I'll just use the old 6 conductor cable to extend this one since then I can match the colour coding.
The lack of that two wire cable so far as cost about $150. I really thought I'd made one and installed it. I guess not.