
Just need a better search statement: https://grabcad.com/library/collet-er-type-1 from "ER20 collet step" query

It makes me realize that 3D printing the collet nut might be more useful than even the collets. Easy way to control the length of the grind.

print collet holders with different depthsBrain fart. Woke up realizing that a custom 3D Printed Holder won't work. It's the gauge depth during setup (for more grind) or during use (for less grind) that has to change, not the holder. A longer or shorter holder won't change the drill grind. It indexes to the gauge set points regardless.
print collet holders with different depths

Why do some drill bits just have a round shank and not the three flats? Even a new/sharp drill just catches and spins in the chuck, without the the three flats
Before I waste money on a sharpener, just toss the round shank bits? Is that a sign of a cheap drill bit?
Round = sign of cheap? Definately not. If I had to guess 90% of drills are round shank, no facets. I'm talking typical machinist /metalworking tooling where they have well established gripping capability; chucks, collets whatever. Only think I can think of with facet shanks is is more utility orientated where you have big holes + small shank ratio and/or generally lower grade chuck retention (hand drills). For sure facet are popular for woodworking (grabby) or metalworking hole saws (high dia: shank ratio) but also weekend warror drills. Nothing wrong with facet. It actually takes more grinding operations to make one (accuratelly) so guessing market-specific? Some (most all?) of the facets I've seen still leave some original round shank surface so I's assume any of the sharpener collets would hold properly on that surface, the facet just isnt used. The sharpener itself sees nothing for torque so shouldnt be an issue?
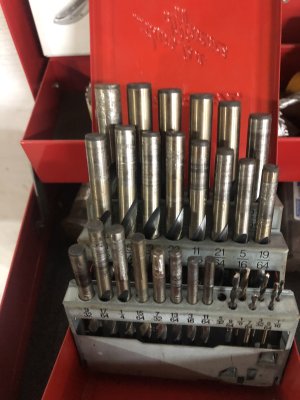
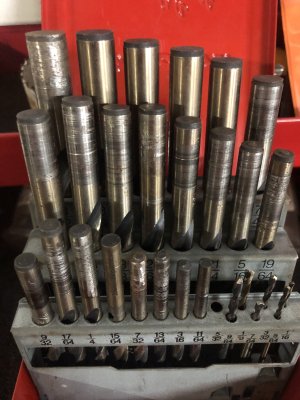 I inherited these, and I'm not sure why the middle four at the back look new, but the rest are all galled. You would try saving these and sharpening them?
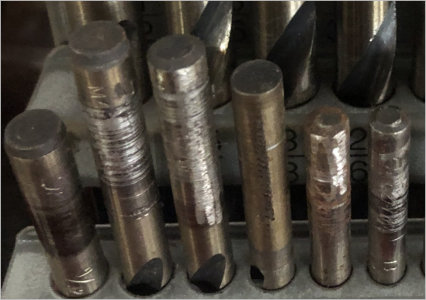

That sounds like a pretty good set to me!There's no part number but they're marked "snap on M42", google came up with m42 is 8% cobalt. It's a 29 pc set, doesn't really tell me if it's cheap or expensive
Good point. Oversight on my part. Makes total sense that the actual drill stickout will be relatively short as a function of the grinder/indexing assembly, so the collet is gripping on the flute lands, not the shank. And I suppose by default, will also deal with any banana axis better in terms of grinding point concentricity, but ultimately the chuck grips the shank so will still come into play if present.As far as a collet based sharpener goes, all of them that I have seen grip the drill by the flutes. So shank defects or hex flats or whatever don't matter.