• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Tool Vevor Drill Bit Sharpener Improved

Tool
The shims are used for web thinning, to lift the bit away from the wheel so the take less of a bite out of a thin web. So only applicable on the A model and D model. Maybe I'll leave the adjustment and try to use larger precision ground guide pins.

Or I'm trying for perfection when I need not? I mean most of my drilling is small diameter work... not a lot of web thinning to be done

I was referring to what Craig did.

Ya, that's a clear issue. It's easy to get carried away. Small Drill are so cheap why bother. Hard to get it right too.

Big drills are the money maker. But hand grinding big drills is a lot easier than small ones. In my mind the machine is best used to sharpen 1/8 to 5/8 drill bits. Smaller is a waste of time and bigger requires a new fatter wheel.
 
This is why I decided on a new separate machine for larger drills.

Maybe that's the best way to go.

In case you have not seen it, here are a few links for your reading pleasure.

Thread 'How to use Vevor Drill Bit Sharpener' https://canadianhobbymetalworkers.com/threads/how-to-use-vevor-drill-bit-sharpener.18908/

 
Late arrival (as usual) on this revisited and interesting topic:
Where are you using shims @CWret ?
I like using a 15mm shim to reduce the standard amount of sharpening - i use it when the bit is not very dull and only needs a touch-up. @Susquatch previously answered that question i believe- he also linked my full discussion on the topic in his post #302 above.

Many months ago - i tested (measured) the reduction in total length of the bit when it was sharpened in a VevorA. I did a std sharpening using 6 bits varying from 1/2” to 13/64” diameter and the sharpening shortened them by 0.018 to 0.025” (depending on how consistently you can set the bit in the collet). Then i sharpened 10 other bits (that varied from 1/2” to 1/4” diameter) and used a 0.015”spacer/shim (to hold the bit away from the grinding wheel, as explained in the above mentioned link). Using the spacer, the bit’s length was reduced by 0.003 to 0.011” by sharpening. Depending on the face angle (118 or 135 degrees typically) the amount of material removed from the cutting face is almost as much as the amount of bit shortening (example: shortening a 118 bit by 0.020” would remove 0.017” from the cutting face). Which is a lot to remove from the bit face if only a little touch-up is needed- so I often use the 0.015 shim/spacer. If necessary, the bit can be sharpened again without the shim, easy-peasy & all with the same set-up. Kinda like measure twice and cut once - but in this case it is grind once, assess and grind again if needed.

- - - -
Using the Vevor A or B with the optionally sourced larger collet holder (and also with larger collets) as Susq discussed above, they can sharpen up to a 3/4” dia bit. But it leaves a little amount on the outer edge that doesn’t get sharpened. I believe this problem is more pronounced on the B than the A - but i have not seen the difference beside each other so this is IMO.
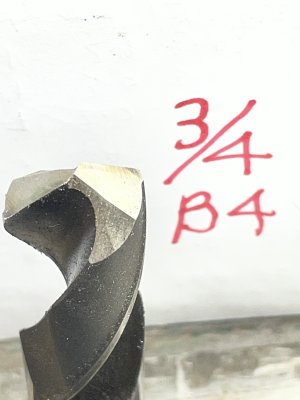
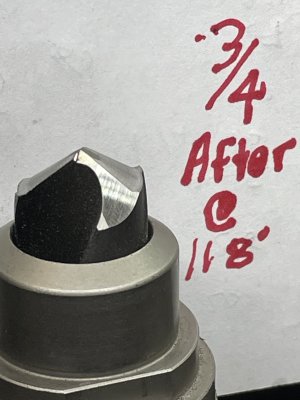
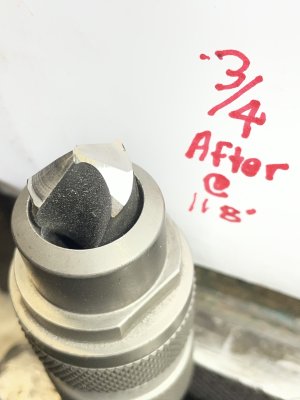
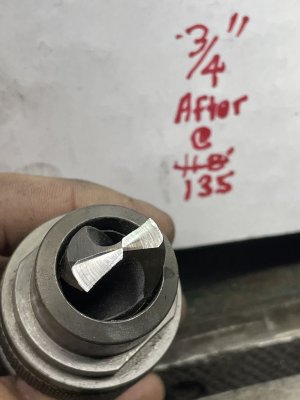
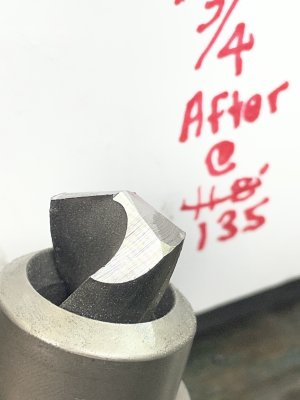
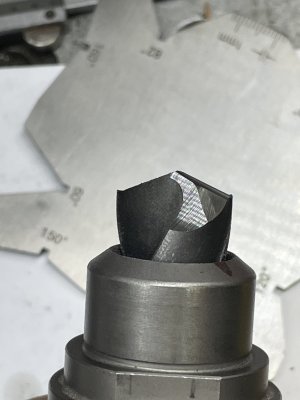
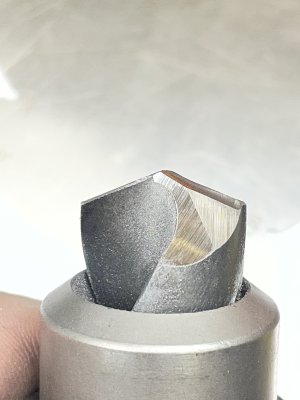
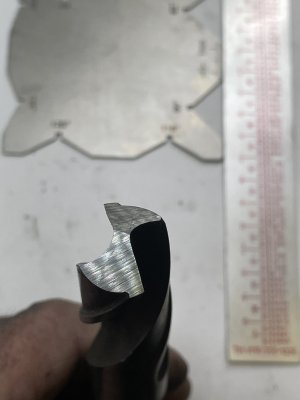
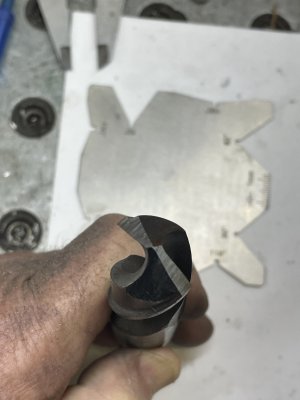
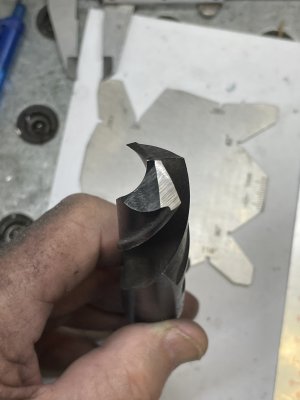
Here’s a 3/4” bit i sharpened today to show the tiny tip of the outer edge that is not removed.
First the before pic:
IMG_7438.jpeg
and after the sharpening (at a 118 angle):
IMG_7441.jpeg
IMG_7440.jpeg
This small unsharpened tip is easily touched up on a bench grinder.
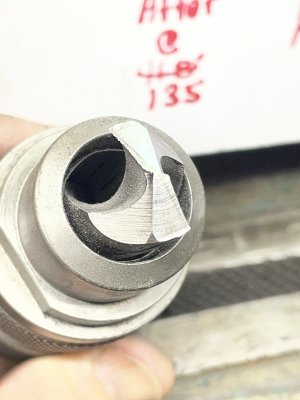
Then i sharpened the same bit again but to a 135 face angle:
IMG_7443.jpegIMG_7444.jpegIMG_7445.jpeg
With the 135 angle the uncut tip is almost gone. It is so small that it was easy to remove with a stone.

PS: I just found this YouTube video that explains web thinning vs a split point grind using a 13A and 13B side by side. Like most YouTube it takes 18 minutes to give 9 minutes of info

 
Last edited:
Where can I get one of these larger collet holders and collets? Is it something Vevor sells?
I have the Vevor B sharpener.

I think you know that I have the B too and Craig has an A.

As Craig says, I got some of the collets on Ali and some on Temu. Some as singles, some as sets.

You can still get the ER25 collet holder on Amazon. But very few sizes of the regular ER25 collets actually work. The collets for the grinder are all held backwards and therefore the skirt or the shank grips are specialized.


Unfortunately the collets themselves seem to be discontinued. I still have them in my shopping carts and should get a notice if they ever stock them again. For now, I think you are SOL.

I posted about them on the grinder thread. They are not intuitive. When I get some time, I'll see if I can improve that advice and post a link to it here.
 
Unfortunately the collets themselves seem to be discontinued. I still have them in my shopping carts and should get a notice if they ever stock them again. For now, I think you are SOL.
I have not read up a lot on these machines....just throwing a thought out there.......could you not make a new collet holder that would use standard cheap collets? Sounds like you might have to figure out a way to turn them around the correct way so you are not using the back of the collet, but it could open up a cheap source for collets and larger sizes.
 
I have not read up a lot on these machines....just throwing a thought out there.......could you not make a new collet holder that would use standard cheap collets? Sounds like you might have to figure out a way to turn them around the correct way so you are not using the back of the collet, but it could open up a cheap source for collets and larger sizes.

I thought about that idea a lot previously. It just seems wrong to have to use inverted collets. After much thought and many tests, I came to accept that the grinder maker made the right choice. Using collets the normal way would have prevented them from fitting the grinder as is. It would have had to be about twice as big as it is and the collet holder would have to have been bigger too. Reversing the collets allows them to stick out as needed to index and sharpen the drills and still leaves room for indexing flats and a recess.

There are probably other ways to do it with a normal collet configuration, but they would "probably" require a different base machine and some limitations. I felt that the exercise of designing such a, system was beyond the scope of what I wanted to do with my machine and probably beyond what others might want too.

Since you recognize this need, I'd suggest that you should explore this for yourself. You might come to a different conclusion that I might have missed. That's just the way such things are. We only know what we know and we only see what we see. The magic of another person is that they look at the same thing but see it differently.

I'm also flagging @CWret on this note so he can comment too.
 
I came to accept that the grinder made the right choice. Using collets the normal way would have prevented them from fitting the grinder as is. It would have had to be about twice as big
Agreed. The path we chose was fairly simple, effective, and not too expensive. I really like being able to sharpen up to 3/4” with a single & easy to use package.

Also - with the use of CBN grinding wheels on my low speed 8” bench grinder - I can do a very good job on sharpening bits larger than 3/4” - and that includes having a good looking split point grind.
 
Ok, so here is a summary of how the ER20 & 25 grinder collets differ from standard collets

Here are the two collet holders with collets installed. ER20 on the left ER25 on the right. You can also see the grinder indexing flats in the photo.
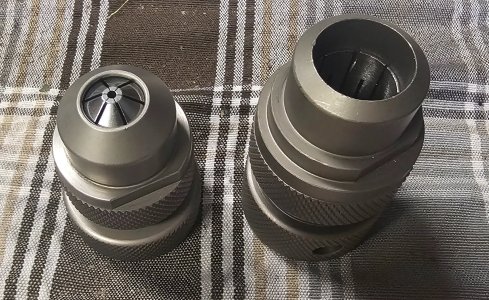
20261002_140339.jpg

You can see the unique nose shapes. Very small for small drills and large for large drills. These are 1/16 and 3/4 respectively.

Focussing in on the ER25 Grinder collets, you can see how the skirt on the 3/4 holder does not reach the holder ID. It is recessed way down inside the holder. If the collet were reversed, the collet retaining grove and closer taper would be compromised. The collet on the left is a standard collet that fits the grinder and any other ER25 collet set. The collet on the right is unique to the grinder.
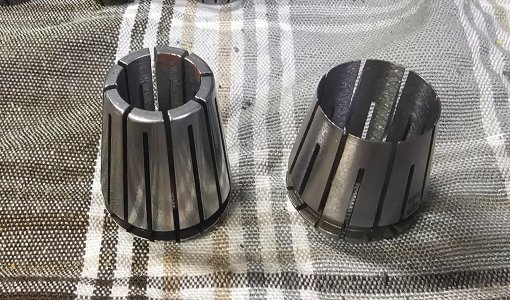
20261002_140603.jpg

The opposite applies to the smaller ER20 collet sizes. A standard ER20 1/8" collet looks like the top right collet from the rear and the top left collet from the front. To make it possible to firmly hold small drills in a reversed ER20 collet, the internal design shown in the bottom collet is modified.
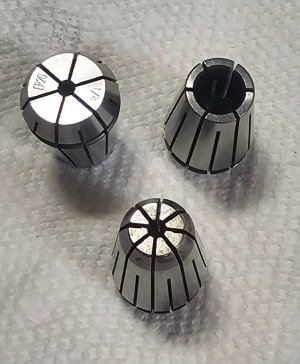
20261002_141120.jpg

Here is a closeup showing the rear of a standard 1/8 collet. You can see the clamping portion down inside. It is designed to hold 1/8 parts at the front of the collet, not the rear. Used in reverse, this collet would not hold a drill bit solidly. Hence the need for the specialized 1/8 collet at the bottom of the photo above.
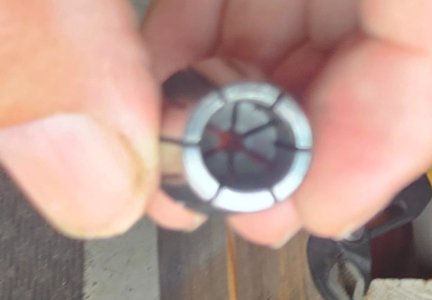
20261002_141257.jpg

To be clear, many of the larger size ER20 collets look like standard collets. So do many of the smaller ER25 Collets.

But buying collets individually isn't generally very economical.

As @CWret pointed out above, there isn't much point in sharpening large drills with the grinder. They are easy to do by hand. Similarly, there isn't much point sharpening tiny drills when they can be purchased at quantities at low cost.

I think the grinder makes sense from 3/32 to 5/8. Even 3/4 is too big and sharpens with a funny geometry in the grinder.

I'm sure there are those who would say that 3/32 is on the small size - better to just buy them in bulk.

 
Oooops - in my above post #303 - I said the bit was 3/4” but it was actually 23/32. My bad.
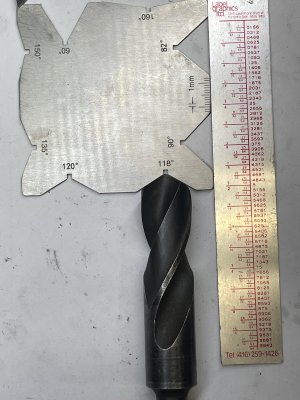
So today i sharpened a 118 degree 3/4” bit to see exactly how much of the tip (outer edge) the 13A does not sharpen. Here’s a pic
IMG_7484.jpegand here after a very quick and easy touch up on a CBN wheel
IMG_7485.jpeg
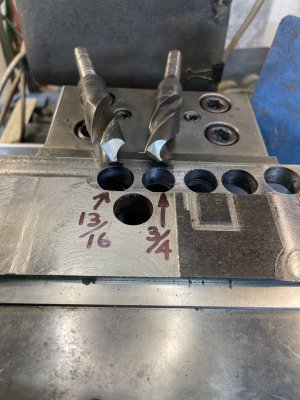
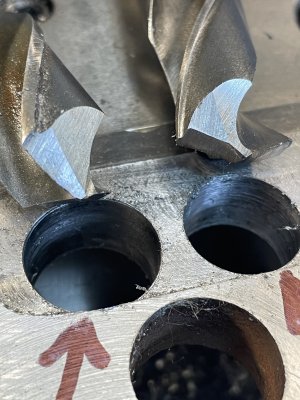
Since the discussion also mentioned hand sharpen bits larger than 3/4” I decided to hand sharpen a 13/16 and compare its performance to a 13A sharpener 3/4” bit.
Here’s pics of the 13/16 after initial hand sharpening:
IMG_7466.jpegIMG_7475.jpegand now pics of the same bit after hand grinding split points:IMG_7481.jpegIMG_7479.jpeg
The proof is in the puddings (as my granny would say) - so i driller a test hole with both the 3/4” 13A sharpened bit and the hand sharpened 13/16” bit. The drill times were almost identical at 45 seconds. The hole quality, effort via down pressure, lubricant, and size of swarf - all being equal. IMG_7491.jpegIMG_7492.jpegPS - thats a scrap piece of 5/8” mild steel that i have used for testing
 
Last edited:
I really like being able to sharpen up to 3/4” with a single & easy to use package.
Thats why I chose the G model for the bit of extra $. Does 3/4" out of the box, nothing more to do. I really wanted to be able to sharpen the bigger than 1/2" drills up to 3/4" that have been sitting since I was gifted a drill doctor 350x that maxes out at 1/2" - that was ages ago so theres been a fair amount of accumulation of those bigger drills.
 
Thats why I chose the G model for the bit of extra $. Does 3/4" out of the box, nothing more to do. I really wanted to be able to sharpen the bigger than 1/2" drills up to 3/4" that have been sitting since I was gifted a drill doctor 350x that maxes out at 1/2" - that was ages ago so theres been a fair amount of accumulation of those bigger drills.

I've had a number of drill doctors. Total crap by comparison. That's all I'm gunna say.

Both the A & B will sharpen 3/4 inch drills if you get the ER25 holder and collets. When I got my B you could get it with and without the big holder and collets. But I am pretty sure they maxed out at 5/8. IIRC, you could only get 3/4 with the expansion collet kit.
 
Back
Top