• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.

Anyone tried the Accusize 5C collet chuck?

In the worst case one can always grind touch up the chuck - I got the cheapest one from China - got it few years ago new for like 150 CAD. No issues. Works great.

I have another one I was given to mount on my other lathe but so far I did not do it.
 
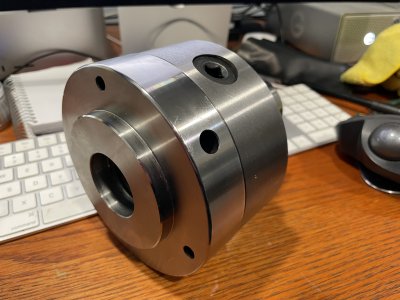
I use the Accusize 5C. As I recall, the backplate supplied by Accusize for that chuck was incorrect, so be careful if you are ordering one.
The Accusize backplate I used was a 5" 1-1/2x8 TPI plain, cast steel version, but the chuck mount holes were incorrect for the 5C chuck which is bolted from the front.


IMG_7492.JPG

No issues with TIR after tuning the fit and nudging it into position.


🙂
 
The front mount chucks are a bit more forgiving to dial in runout to the backplate, BUT, more details to discuss here. My original Bison integrated (non-SetTru) 5C actually wasn't all that great, about 0.0015" TIR. I cant recall what the factory specs were but I wanted better. And that TIR was on a preferential D1-pin orientation (which you should always repeat). That's the end of the trail for a direct mount chuck. You cannot (easily) disassemble an integrated chuck even though seeing 3 front screws might lead you to believe that. They are factory pressed & gronked.

If you get a plain back 5C chuck designed to mount to variety of backplates like some of the Asian models, you might be able to use this to your advantage. As long as the face lip / mount is not too tight you could shift the chuck to null runout & lock it in place. The issue is, it really SHOULD be a snug fit or its probably going to drift eventually. Maybe if you are brave, turn off 0.002" from the backplate boss & insert shims onto the quadrants. Like 0.0030" at 12:00 & 0.005" at 6:00 gets you 0.0025" net displacement. That kind of thing. Tune-able to 2 axis.

Now none of this speaks to the 5C taper collet face. If the chuck arguably runs true to spindle center but the seat is ground slightly eccentric, its still going to have problems. Thats why I like to put an indicator directly on the seat to get confirmation. Adding a questionable collet + questionable dowel is further aggravating the issue, so have to do this step by step

 
Thats why I like to put an indicator directly on the seat to get confirmation. Adding a questionable collet + questionable dowel is further aggravating the issue, so have to do this step by step

^^ This! There are wild differences between collets. It is imperative to test the collet seat first.

Tip - I've seen pictures posted with an indicator ball sitting on the seat such that rotation pulls the indicator ball sideways. This can introduce error of its own. I always position the indicator such that rotation drags the ball mostly away from the indicator with little to no sideways force.
 
Super cheap chucks. First one bad, returned, second fine.


Craig
 
Back
Top