• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

Hi Michael,

Sharp tools and less speed. I would have thought 150 to 300 RPM. Carbide inserts are not the best for cutting threads in brasses.
What feed and speed did you use ? Or if its a common thread a run over with a die might clean it up or make it too small.
 
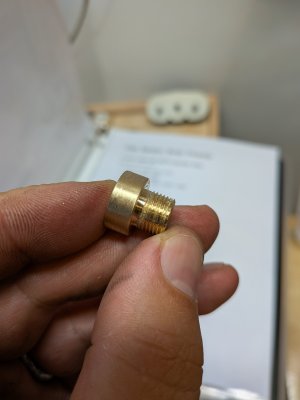
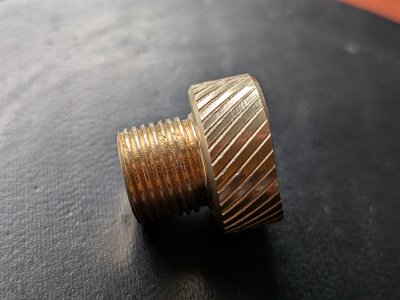
I see some shrapnel hanging off the edges..... a couple things come to mind.
Sharper tool
Lighter cuts and more passes
Tailstock support, Its evidence can be removed at the end, just leave a length provision for that.
Clean up with a light filing and emory at the end.
 

This little gem in the rough is probably worth inquiring about...... I have been mulling it over for awhile. If you look closely it's a tool grinder lying on its side with one table missing. It could be a game changer.

Yes...... I surrendered and joined facecrack.
 
What feed and speed did you use ?
70 RPM if the manual is to be believed!

Sharper tool
Yes I'm looking for some other options. I've had better results with some of my inserts, this was a single piece carbide.

Lighter cuts and more passes
This was... 5 passes: .005x3, .002x2

Tailstock support, Its evidence can be removed at the e
Because of some shenanigans I didn't think I could, but now I realize I actually can, so that's on the list!

Clean up with a light filing and emory at the end.
Did not do any clean up, will have to see what I have on hand for next time.
 
Hi Michael,
A file will remove most if not all surface debris, but using a stone will give it a polish.
I think that your thread cutting tool wasn't sufficiently sharp, a problem with general carbide inserts. Ones intended for aluminum are much sharper and will provide a better finish. They also cost a little more !
 
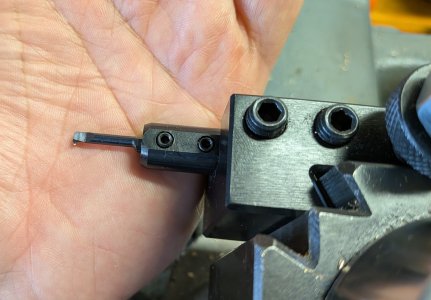
I do think the tool is a likely culprit. I was using a different kind (attached). I had cleaner results with an aluminum insert in a different holder, but I need to find one that is small enough to work in a <0.400" bore...
 
Hi Michael,
The only way you are going to get a threading tool into a 0.40" thou bore is to make your own from HSS !
Or use a tap the right size and grind half of it away so that you have a tool that will cut and go inside your bore. I've salvaged a tap that I've broken before now to thread a very small hole.
 
Hi Michael,

By gum that looks like a flimsy tool ! Its going to chatter no matter what you do with it.
You could try wrapping some plumbers lead solder wire around the shaft in an effort to damp the chatter out.
 
Back
Top