• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

You can turn tapers under power by setting the tail stock over, can even turn long tapered threads that way, LOL.
Just resetting the tail stock can be a bit of a pain. There is or can be made a set over attachment to put in the tail stock spindle so the tail stock does not need to be moved sideways.
Typed whiles faster fingers were typing.
 
If I had to cut a lot of tapers I'd get one of these:
Oh that's interesting. I may have to look into that. At least to try it out! Ah, I'll need MT2

Would that need a dead center (headstock) with a different tip or tip angle to properly drive the work? Research time

I'm only tapering up to about 3° currently.
 
Amazingly I have most of that list! Taper attachment would be so nice for cutting tapers under power
If the taper that you're cutting is generally the same as is the length of the material, you could offset your second tailstock for the correct taper and swap tailstocks as required. The parts will have to be turned between centers, but if you make a 60° center to clamp in the chuck and face it each time before use, you won't need to keep swapping the chuck out as well as the tailstock. Drive the lathe dogs off the chuck jaws.......
 
If the taper that you're cutting is generally the same as is the length of the material, you could offset your second tailstock for the correct taper and swap tailstocks as required. The parts will have to be turned between centers, but if you make a 60° center to clamp in the chuck and face it each time before use, you won't need to keep swapping the chuck out as well as the tailstock. Drive the lathe dogs off the chuck jaws.......
I need to service that tailstock still. But that is a perfect use for it!
 
Hmm, might be why some lathes have no tail stock. Some people have two tail stocks per lathe. This may mean some have more then 2 per lathe?!
 
I would count having two tail stocks as a taper attachment for sure.

Dialing in a tail stock to cut square takes a bit of fiddling, and I don’t want to do that every time.

A taper attachment just separates the taper turning function from the tail stock function and makes it a lot more user friendly as you can perform other operations while still holding the same taper in reserve.

Again, that list doesn’t count specialty stuff, or metrology. I have a bunch of “specialty” tooling that isn’t for general purpose work that I consider essential.
 
Dialing in a tail stock to cut square takes a bit of fiddling, and I don’t want to do that every time.
Exactly why I'm not enthused by it.

I will need to figure out how much offset gives me the desired tapers and how best to switch between them. Again that's where the compound or one of those MT assemblies seem nice, just dial in the number on the scale.
 
Yup, folks bogarting tailstocks, that accounts for tailstock-less lathes. ;-)
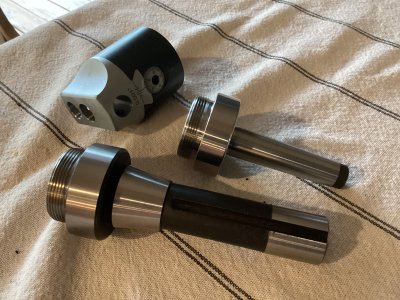
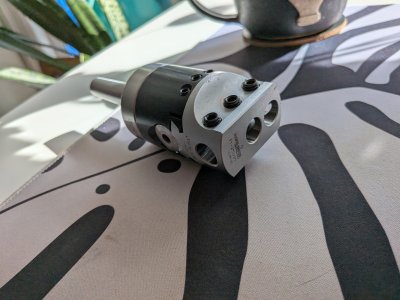
Just buy a boring head with a MT2 male end and use it for the offset, easy peasy.
 
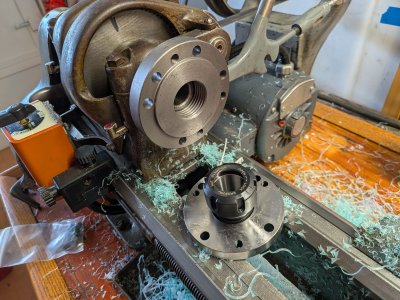
Correct. This is my 2” offset boring head with MT 2 & R8 screw on adaptors. Pretty cheap on amazon.
I would use a 1/2” center in this, or some such, or be creative.
Set it up with your desired offset, then lock the tailstock quill & proceed.
 

Attachments

  • IMG_2361.jpeg
    IMG_2361.jpeg
    2 MB · Views: 3
Keep in mind the set over amount will change with the distance between centers.
That’s one advantage of the taper attachment. Same taper no matter the length between centers. Drawback: sometimes the taper attachment isn’t long enough and you have to do in multiple steps.
 
Hi Michael,

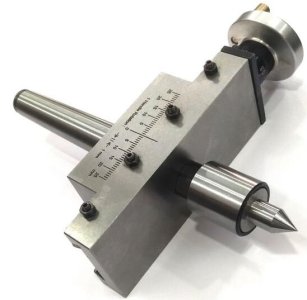
A picture of my tail stock taper attachment.

Taper Turning attachment.jpg
I actually made one of these but can't find the pictures at the moment. Note that the rotary center is not supplied with the tool.

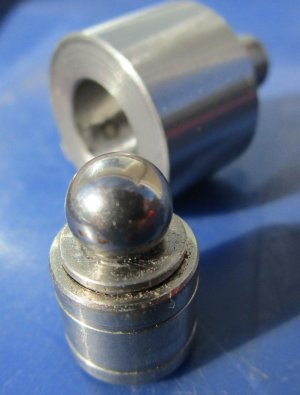
30-09-2025-006.jpg
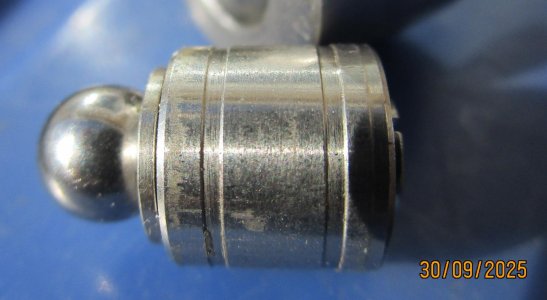
30-09-2025-007.jpg

This is what is needed, a ball center. This one is a salvaged 12 mm bearing pack from a computer hard disc drive with a 6 mm diameter steel ball glued onto the end. This works far better than a cone center because the cone pushes the work off to one side, whereas a ball allows the work to rotate freely.

And last a PDF of a taper attachment.
 

Attachments

Yep I've got the accusize one! Just need a center. And to figure out the other end.
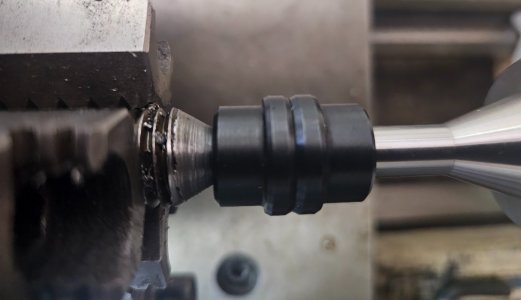
Yes, those work. I use one sometimes. You can buy small live centers on Amazon and add a bushing to fit your boring head.


The other end is really easy! Any old piece of stock will do. ALWAYS cut headstock centers in place. This insures perfect concentricity. Doesn't need to be great stock. Even an old bolt will do. Just set your compound to 30 degrees and cut it. As long as you leave it exactly where you cut it, it will always be perfect. I think many of us do this routinely. It's a very standard old lathe trick that all lathe users should know. The one on the left in this photo is a good example. Even though it's made from an old crappy threaded bolt. It is a dead nuts perfect center because it was cut in place on my lathe.

Buttons Vertical View (1).jpg
 
Back
Top