• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

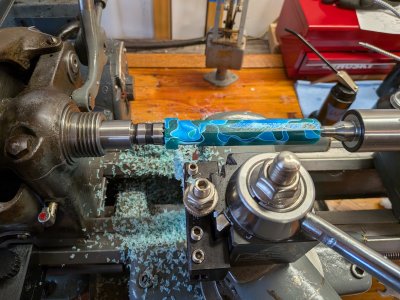
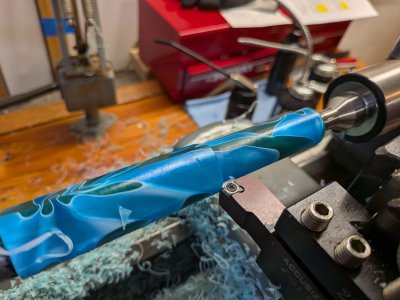
Working on my South Bend 9C

What about using a Steb center instead of the dead center/dog/drive plate assembly?

I suspect the answer is "try it and see", but if anyone sees a red flag....
 
What about using a Steb center instead of the dead center/dog/drive plate assembly?

I suspect the answer is "try it and see", but if anyone sees a red flag....
I don't know a lot about wood turning but my understanding is that on a metal lathe we use a drive dog because the taper fit in the spindle alone shouldn't be relied upon to drive work, like when my tailstock chuck slips and rotates with those deming drills. . .
Can you force the steb center to spin without slipping would be my question . . .
 
I'm also a wood turner. A Steb centre should be just fine as a drive centre for small diameter work. If you have a spur drive it would also be fine as they are purpose made for spindle turning.
 
I think the drive dog was/is more to do with material to large to go in a chuck, and that many early lathes did not have a chuck or even a hole through the spindle. The chuck as we know it, is a fairly recent addition to the lathe history. Some lathe users have never used a face plate or even turned between centers.
 
That looks like it works pretty good.

If you ever get into more “general” fab and machine stuff, or for certain other instances, four jaw chucks are absolutely invaluable.

It’s still worth keeping your eyes peeled for a suitable four jaw to scoop up opportunistically.

No lathe is “fully tooled” without at least one four jaw. I have three.
 
Well baitmster you say a lathe is not fully tooled without a 4jaw. I say is a lathe ever fully tooled.
Haha fair enough.

The closer you get to fully tooled the further away you realize you are…..

There is a point though where a lathe is tooled enough where if you were purchasing it you would consider it generally fully tooled…..

I guess fully tooled to a point.

I would consider, if purchasing:

- 3j
- 4j independent
- collet chuck w/ common assorted collets
- face plate and dogs
- all necessary change gears for metric/imperial and feeds
- steady rest and follow rest
- dead, live, and headstock centers
- quality drill chuck for tail stock
- taper attachment if it has the capability
- quick change tool post and a good number of holders
- carbide holders to suit, an assortment. (You may not have everything you want, but an assortment is good enough to get you started)
- hss holders and blanks, parting blade holder.
- solid lathe stand that allows alignment/levelling.

Fully tooled.

Everything else I would consider to be “extra” or specialty, or to do with metrology and not something to do with the lathe.

There’s always another gizmo or gadget to add though I agree.

 
Hi Michael,

A taper attachment is nice and a useful device to have, but you will have to set to and make one, particularly if you make the shape follower guide as well.
 
Hi Michael, I agree I wouldn't pay that amount for one . But they are not that difficult to make. There are designs kicking around.
 
Back
Top