• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

Boom sticks & pond ducks.
Wandering thread?
This all began way back when........ @Golem Pens first detected a significant amount of runout on one of his pens, that little wobble oh so many posts ago has become a serious whip now that we're so far from the initial source. So technically I think we are still on topic, and this is a good reminder how important a true running lathe is to keeping the universe in order..... 🙄
Nope, just a bit of crosswind. lol
......... or this. ^ 😉
 
Hi Guys,

Even with a true running lathe, the problems start with changing the conditions during the turning of a part. The more of a job you can complete at one setting the less runout between parts will result.
Take the threading between internal and external on a single part. Once you alter the setup any
co-axialality disappears.
 
Yes, I'm aware. Which is why I aim to run the multi-step operation of tenon shaping > external die > internal bore > internal tap all in sequence without removing the piece from the chuck.

Not that there isn't a better method, or that there isn't something in my tools or set up that that isn't skewing things. But I AM trying to address the considerations of co-concentricity. Specific recommendations may be helpful.
 
My personal recommendation is to get one with a belt at least.

I’m considering selling my 6” wheeled bench grinder now that I have my 2x72 belt grinder.

The belt grinder is like, far and above superior to any bench grinder I’ve ever used in my life. Not even a fair comparison.

Some guys say a big 10” one is comparable power wise, but one thing that is on a different level is how easy it is to change grits, and get different belts and change them. Takes 2 sec.

Power wise the belt grinder still is above anything I’ve used or seen.
 
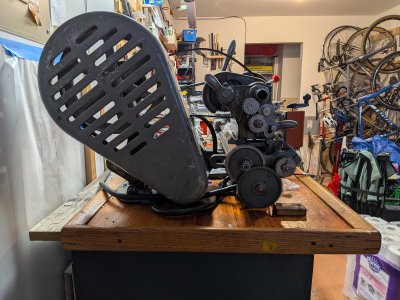
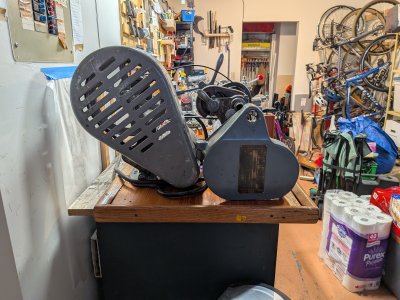
Finally getting the change gears mounted up so I can play around and ope, as I feared there isn't clearance between the motor pulley cover and the gear cover! Motor cover will have to come off to run gears
 
It's a problem with horizontal rear drives like that, because they take up so much space folks tend to squeeze them together too much.... If you can raise the drive up onto a pedestal about 12" or 300mm for you young whipper snippers, you should be able to get the clearance. This space conundrum is why I went overhead on the 13".....
 
Yeah I simply don't have more horizontal space available. Wasn't an issue before I had the motor cover 😉

Hmmm I could get it up higher, though I would need a longer belt in that case.
I think some wise man once said " for every action, there's a reaction "
Yes, you will likely need a new belt and all the fun that entails.... I am very happy with the serpentine belt that I cut to length and joined the ends together with a belt clipper...... when is the last time the wifes car got a new fan belt? Nudge nudge....
 
Back
Top