• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

South Bend lathes don't want MT tapers if I recall correctly
The 9" does in fact have mt3 in the spindle. It would normally use 3c collets with an adapter, whereas the 10k takes a 6k collet directly in the spindle..... I can't imagine what one might be doing that would bend a spindle and not leave lasting scars somewhere.... I think it's time to slow down an take a measured approach to finding the error.
@Golem Pens , can you get us a picture of how you are measuring the run out? Is it being taken from the spindle directly? Or the collet chuck?
Right, my 10K took 6K collets which were very expensive.
Research seems to indicate that MT3 collet don't fit properly.
 
Hi Guys,

Some people have reamed the spindle to take MT3 tooling ! But you do need to make sure that the spindle and bearings are tight and properly set up. No point in reaming or boring the spindle if it has any play in it, the spindle has to be right first !
 
My guess is the MT3 taper is fine, the SB9 spindle is pretty robust, it would be hard to bend with use.
This is a collet chuck, meant to be very accurate, my opinion is it needs to be more accurate than a threaded-on collet chuck.
Even a cheap dial indicator or DTI will show movement on the on the spindle.
And i could be wrong, but i don't think so.
The usual test is to put an indicator on the spindle and clamp a bar in the chuck. Pulling and pushing on the bar will show if there is any spindle wear.
 
What are the spindle bearings? Babbet or ball/roller, I likely have missed it in the posts, though by the oilers and the split caps I am thinking babbet. If so, are there any shims that maybe removed to snug the spindle up abit?
 
The usual test is to put an indicator on the spindle and clamp a bar in the chuck. Pulling and pushing on the bar will show if there is any spindle wear.
But, I think I have been reading play and run out being interchanged and I think we need to start from the beginning and methodically asses things a little better before fixing anything.... 😉
.....and this coming from a guy that usually takes the shotgun approach to repairs.
 
But, I think I have been reading play and run out being interchanged and I think we need to start from the beginning and methodically asses things a little better before fixing anything.... 😉
.....and this coming from a guy that usually takes the shotgun approach to repairs.
You are dead on. Lots of good information shared, but on varying topics. I'll document my findings with pictures when I get a chance today
 
Okay let's start at the start (well, not where I started, but at the core).

Longitudinal spindle play is ~.001" which is to spec, so no issues here. Ajusted with the spindle take up nut (I added the thrust bearing mod). This is with the headstock bolts loose (more on that later). No photo.

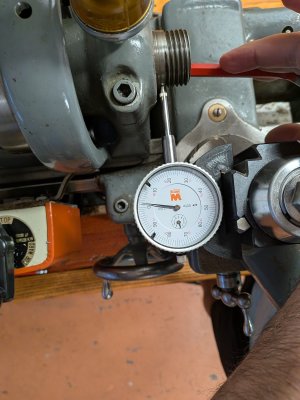
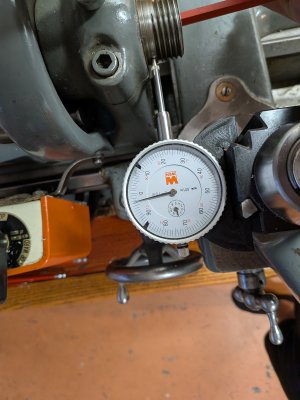
Lateral spindle play using the SB method (ish - I can't mount an indicator at the top of the spindle, so I checked laterally). ~.002" in one direction and ~.004" in the other, which is out of spec (.001-.002 I believe is the target). This is with the headstock bolts barely snugged up, since under any appreciable tension the spindle binds. This is a problem, and I almost wonder if additional shims are needed instead of fewer.

1000004841.jpg

1000004837.jpg

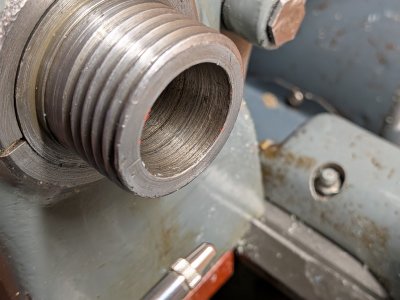
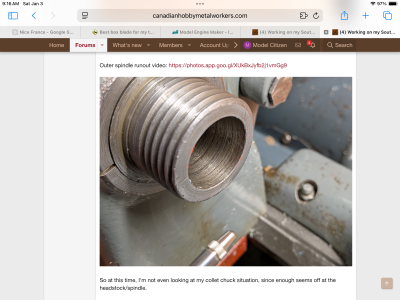
Spindle runout. The outer surface isn't smooth so I don't trust it. The interior is rough and ridged, so I suspect it has been bored out in the past... I'm not sure how to get an accurate read on spindle run out based on this.

Outer spindle runout video: https://photos.app.goo.gl/XUkBxJyfb2j1vmGg9

1000004840.jpg

So at this time, I'm not even looking at my collet chuck situation, since enough seems off at the headstock/spindle.

Thoughts on this?

It SEEMS I should try and take up spindle play, but tightening that down binds the spindle before adjusting play.

I can of course disassemble the spindle assembly again for a closer look...

 
Okay let's start at the start (well, not where I started, but at the core).

Longitudinal spindle play is ~.001" which is to spec, so no issues here. Ajusted with the spindle take up nut (I added the thrust bearing mod). This is with the headstock bolts loose (more on that later). No photo.

Lateral spindle play using the SB method (ish - I can't mount an indicator at the top of the spindle, so I checked laterally). ~.002" in one direction and ~.004" in the other, which is out of spec (.001-.002 I believe is the target). This is with the headstock bolts barely snugged up, since under any appreciable tension the spindle binds. This is a problem, and I almost wonder if additional shims are needed instead of fewer.

View attachment 75850

View attachment 75851

Spindle runout. The outer surface isn't smooth so I don't trust it. The interior is rough and ridged, so I suspect it has been bored out in the past... I'm not sure how to get an accurate read on spindle run out based on this.

Outer spindle runout video: https://photos.app.goo.gl/XUkBxJyfb2j1vmGg9

View attachment 75852

So at this time, I'm not even looking at my collet chuck situation, since enough seems off at the headstock/spindle.

Thoughts on this?

It SEEMS I should try and take up spindle play, but tightening that down binds the spindle before adjusting play.

I can of course disassemble the spindle assembly again for a closer look...
Yikes...... I think I see why it came with a new spindle.... the inside taper. It should be smoothly ground in there.... yes, you will need to sort out the shims, as those bolts want to be tight.
 
@140mower fantastic, the confirmation is appreciated! I'll open up that backup spindle and take a look, and plan to tear down the spindle assembly for a closer inspetthere too. I may be out of suitable shim stock...
 
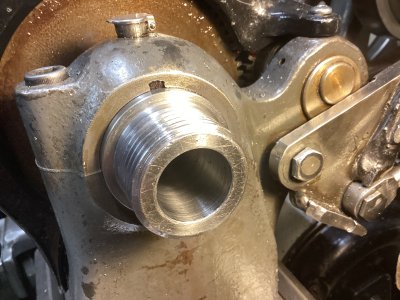
WOW! The photo on left is my ‘36 spindle.
How far have has it been bored out?
Does it still have a smooth MT3 taper deep inside?
EDIT or has something spun inside & galled?
 

Attachments

  • IMG_2157.jpeg
    IMG_2157.jpeg
    2.2 MB · Views: 9
  • IMG_2158.png
    IMG_2158.png
    2.7 MB · Views: 9
WOW! The photo on left is my ‘36 spindle.
How far have has it been bored out?
Does it still have a smooth MT3 taper deep inside?
EDIT or has something spun inside & galled?
Hi Guys,

That looks like its been bored with a blunt tool.
My thoughts are that it needs a ream out with a proper MT3 reamer !
Then you can run your dial gauge on the rim of the bore. I would also suspect that the tool used wasn't even on centre, or cutting height.
 
Yikes...... I think I see why it came with a new spindle.... the inside taper. It should be smoothly ground in there.... yes, you will need to sort out the shims, as those bolts want to be tight.
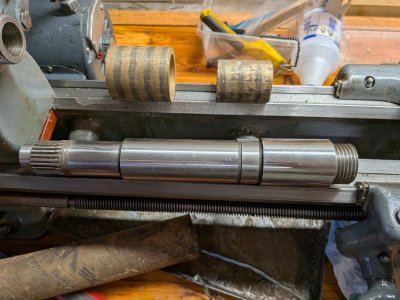
Replacement piece looks a lot better. But, gonna see if I get anywhere with shimming the current one before doing a swap.
 

Attachments

  • PXL_20260103_180246096.jpg
    PXL_20260103_180246096.jpg
    1.7 MB · Views: 13
Back
Top