• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.

METAL LATHE SMOKE, RPM LOSS, NEW LATHE MOTOR?

just ordered the new motor and vfd, lots of real world experience here, pretty amazing actually. E Motors Canada was really helpful and as I understand it knows this forum quite well.

ps......
I actually thinks some of these guys are only here to help spend other guys money as their own wives have their credit cards locked tighter than a Medieval Chasity belt, I think it's working to be honest.....😉
Only offering because susq tagged me a bit back.

If you’ve got it figured, then all good.

The other guys around here and MORE then dangerous when it comes to VFDs and also spending other guys’ wives money.
 
Only offering because susq tagged me a bit back.

If you’ve got it figured, then all good.

The other guys around here and MORE then dangerous when it comes to VFDs and also spending other guys’ wives money.
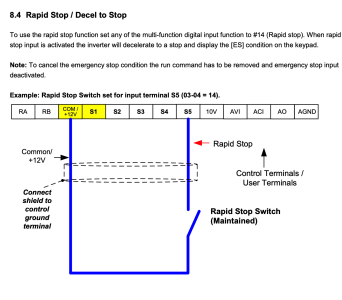
I have watched Cloug42's videos on his vfd series, the problem, not in a bad way, is where does a guy call it quits, contractors, more breakers, filters, 12 power supply and so on. his initial set up with the vfd with the addition of a pot and three pole switch for speed and fwd/rev is really all I need with the addition of another breaker in the job box just because.
 
Some of these repossess are pure Greek to me, but I consider electricity black magic. They talk of VFD compatible, that adds a fair bit to the cost of a 3 phase motor. Used 3 phase motor can be had cheap enough, I paid $20 for my 2hp Baldor, though that was a great deal off Craig's List. Older motors predate VFD, but quality motors are quality motors, they just don't have a VFD tag. The main problem mentioned is the cooling fans run at motor RPM , since VFD changes RPM, you can see the problem. I limit my frequency range change.
 
Some of these repossess are pure Greek to me, but I consider electricity black magic. They talk of VFD compatible, that adds a fair bit to the cost of a 3 phase motor. Used 3 phase motor can be had cheap enough, I paid $20 for my 2hp Baldor, though that was a great deal off Craig's List. Older motors predate VFD, but quality motors are quality motors, they just don't have a VFD tag. The main problem mentioned is the cooling fans run at motor RPM , since VFD changes RPM, you can see the problem. I limit my frequency range change.
Hi DW2,

Industrial motors are sometimes run 24/7 and need to be kept cool, at least not allowed to overheat hence the separate motor driven fans. These are usually mounted on the rear of the motor but sometimes inside the case.
 
They talk of VFD compatible, that adds a fair bit to the cost of a 3 phase motor. Used 3 phase motor can be had cheap enough, I paid $20 for my 2hp Baldor, though that was a great deal off Craig's List. Older motors predate VFD, but quality motors are quality motors, they just don't have a VFD tag. The main problem mentioned is the cooling fans run at motor RPM , since VFD changes RPM, you can see the problem. I limit my frequency range change.

So this is where we get all messed up on the subject of VFDs.

A VFD will work with almost any 3 phase motor that is compatible - and that is almost everything.

An optimum install includes a VFD Rated motor. 10 and 20 turn down motors can be had for low cost too. They are just harder to find, and new ones are expensive.

Like most machinery in our hobby shops, it's really only about how patient you are.

Why be patient when you can get a motor tomorrow that will work just fine. I guess that mostly depends on how low you want to run your motor.

A regular motor will be find at 45 Hz and even lower if you are careful. But a 10 turndown motor will run fine at 6 Hz! If you need a motor that will run fine at 6 hz, you need patience. Not much more to it than that.

And never ever forget that you can't run at 6hz at full rated hp. That won't work. What you can do is run at full torque - as long as you accept that you cannot have full chip load. You can't have big chips on big diameter parts. For that, you need gearing. I don't need big chips but I do want low speed at high torque to thread SS smoke poles.

That's prolly clear as mud. But I do hope it helps.
 
So this is where we get all messed up on the subject of VFDs.

A VFD will work with almost any 3 phase motor that is compatible - and that is almost everything.

An optimum install includes a VFD Rated motor. 10 and 20 turn down motors can be had for low cost too. They are just harder to find, and new ones are expensive.

Like most machinery in our hobby shops, it's really only about how patient you are.

Why be patient when you can get a motor tomorrow that will work just fine. I guess that mostly depends on how low you want to run your motor.

A regular motor will be find at 45 Hz and even lower if you are careful. But a 10 turndown motor will run fine at 6 Hz! If you need a motor that will run fine at 6 hz, you need patience. Not much more to it than that.

And never ever forget that you can't run at 6hz at full rated hp. That won't work. What you can do is run at full torque - as long as you accept that you cannot have full chip load. You can't have big chips on big diameter parts. For that, you need gearing. I don't need big chips but I do want low speed at high torque to thread SS smoke poles.

That's prolly clear as mud. But I do hope it helps.
At first It was lack of skill/knowledge and l was cautious on replacing the motor and adding a vfd. It's not a lack of wanting to learn something new, it's quite simple, I don't want to make things worse and spend money on stupid mistakes fumbling around with something and creating more smoke. I like proper direction and someone who has the patience to explain even the dumbest of questions I may have, yes over and over again if necessary. Yah I was a really crappy student in skool, trying to find someone to explain things in a way I could understand is actually very difficult, I know my wife is a teacher.

Thank you all
ps, parts are on the way, anyone want to see pics of the burn marks after I'm done??
 
just ordered the new motor and vfd, lots of real world experience here, pretty amazing actually. E Motors Canada was really helpful and as I understand it knows this forum quite well.

ps......
I actually thinks some of these guys are only here to help spend other guys money as their own wives have their credit cards locked tighter than a Medieval Chasity belt, I think it's working to be honest.....😉
$hit...... He's on to us boys. 😱
 
Well the parts are slowly arriving and I have a plan in my head on the external controls along with starting to put switches into the new face plate, noting fancy just practical.

I do have a lathe operation question and I thought since this is a fresh conversation I'd post it here as the same members weighed in on the lathe when I brought her home.

Before the smoke appeared....😉. I was trying out different cutters to get the nicest cut along with different spindle speeds. So when I turned the speed up on steel I engaged the auto feed (not the lead screw) and began the cut. The cut was quite nice and shiny at the higher rpm's.

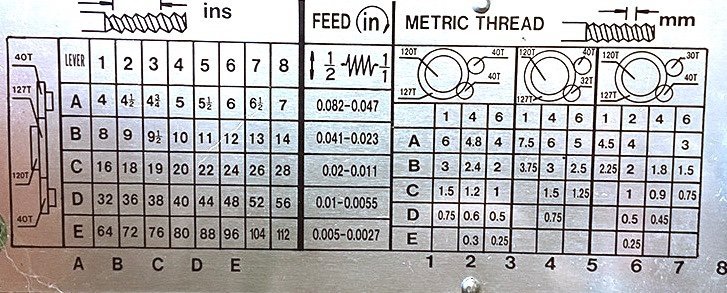
Q: is it correct to engage the gears on the threading gear levers to control the speed of the cut?

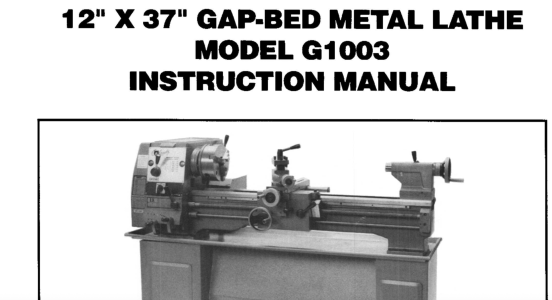
This may seem like a dumb question but I don't see any other way to have high rpm's and a slow auto feed rate to produce nice cuts. I do have the Grizzly manual as this machine has many names and variations but it really doesn't say too much.

cheers.

ps.
pictures to follow on the repairs shortly.
 
Well the parts are slowly arriving and I have a plan in my head on the external controls along with starting to put switches into the new face plate, noting fancy just practical.

I do have a lathe operation question and I thought since this is a fresh conversation I'd post it here as the same members weighed in on the lathe when I brought her home.

Before the smoke appeared....😉. I was trying out different cutters to get the nicest cut along with different spindle speeds. So when I turned the speed up on steel I engaged the auto feed (not the lead screw) and began the cut. The cut was quite nice and shiny at the higher rpm's.

Q: is it correct to engage the gears on the threading gear levers to control the speed of the cut?

This may seem like a dumb question but I don't see any other way to have high rpm's and a slow auto feed rate to produce nice cuts. I do have the Grizzly manual as this machine has many names and variations but it really doesn't say too much.

cheers.

ps.
pictures to follow on the repairs shortly.

Hi MM,

On my Myford lathe the gearbox setting controls the power feed speed. The power feed speed is also changed according to the spindle speed.

So the spindle speed would be set according to the diameter and material that you wanted to machine, then the gearbox would be set according to the amount of cut you wanted. In my case the finest cut would be 0.2 thou per rev/turn of the chuck. This 0.2 thou would be constant per rev ( each turn of the chuck would move the saddle 0.2 thou )

HTH.
 
Q: is it correct to engage the gears on the threading gear levers to control the speed of the cut?

Lathes come in many different designs. To answer your question, I would need to look at your lathe or its operating manual. I don't recall what you have. Could you please remind us what model it is and what grizzly model is the same?

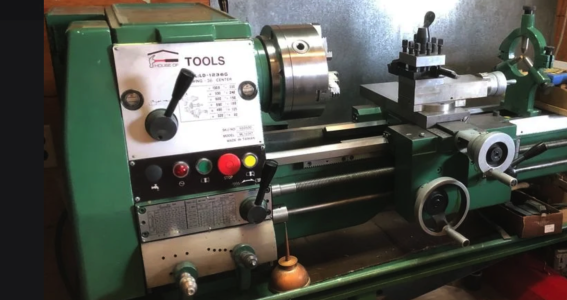
But for reference, on my grizzly lathe there is a lever that is used to switch between threading and feeding and another lever that switches between neutral, cutting feed (carriage), and facing feed (cross-slide).
 
Lathes come in many different designs. To answer your question, I would need to look at your lathe or its operating manual. I don't recall what you have. Could you please remind us what model it is and what grizzly model is the same?

But for reference, on my grizzly lathe there is a lever that is used to switch between threading and feeding and another lever that switches between neutral, cutting feed (carriage), and facing feed (cross-slide).
The closest reference is the Grizzly G103, looks identical. I just want to make sure I'm not missing something when using the power feed, I disengaged the threading gears and ran a test and no feed when I first got her home so logic would say the threading gears need to be engaged.

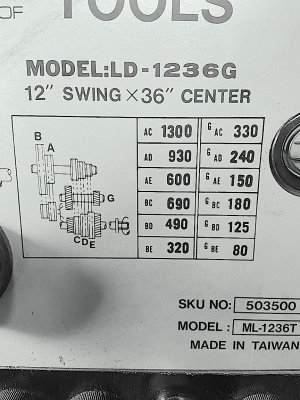
I am trying to weed out a coincidence, smoked the motor at top speed because it was ready to fail or did I put too much strain into the motor with a slow feed rate and high speed, I am leaning towards a tired motor.
 

Attachments

  • Taiwanese_ML1236T_Thread_Table_WEB.jpg
    Taiwanese_ML1236T_Thread_Table_WEB.jpg
    87.4 KB · Views: 4
  • Taiwanese_ML1236T_Spindle_Speed_Table_WEB.jpg
    Taiwanese_ML1236T_Spindle_Speed_Table_WEB.jpg
    249.6 KB · Views: 3
  • Screenshot 2025-09-19 at 9.25.01 AM.png
    Screenshot 2025-09-19 at 9.25.01 AM.png
    788.5 KB · Views: 4
  • Screenshot 2025-09-19 at 9.26.39 AM.png
    Screenshot 2025-09-19 at 9.26.39 AM.png
    1.6 MB · Views: 4
Back
Top