-
Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
-
The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.
You are using an out of date browser. It may not display this or other websites correctly.
You should upgrade or use an alternative browser.
You should upgrade or use an alternative browser.
Working on my South Bend 9C
- Thread starter Golem Pens
- Start date

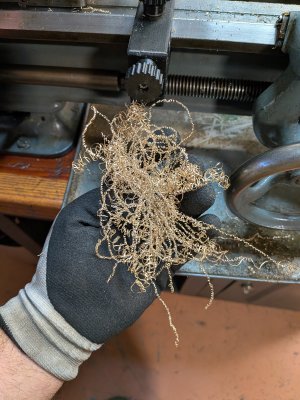

We're having fun, making danger ribbon.
You do seem to like working on long skinny stuff. Why brass instead of steel?
Golem Pens
Michael
This is still all the same dang piece. I've only been able to snag 5 minutes now and then to work on it.You do seem to like working on long skinny stuff. Why brass instead of steel?
Brass vs steel, no particularly GOOD reason. It's what I have on hand, is what other folks tend to use for these mandrels, I'm not sure how the obnoxiously expensive triple start dies will do with steel.
I'm not sure how the obnoxiously expensive triple start dies will do with steel.
Two words for steel or brass.....
"SINGLE POINT"
Doesn't care how many starts.
Does a superior job.
Is totally adjustable.
Is virtually free.
Generates significant pride.
Could be an advertising feature.
Admiration of Forum members.
More fun than a pink yoyo.
Golem Pens
Michael
I knowwwwww and I want to. I need someone to sit down and help me figure it out. It would be a MASSIVE change to my production workflow.

140mower
Don
The " How to run a a lathe " book by south bend describes the process very well. I haven't tried multi start threads, but the process is well layed out, and is what got me over the hurdle to threading on the lathe. If you haven't picked up a fish tail gauge yet and thread gauges, do so, as they're cheap like me....I knowwwwww and I want to. I need someone to sit down and help me figure it out. It would be a MASSIVE change to my production workflow.
Try not to wait too long to start cutting threads, it's way easier than you think. Turn down a short section of scrap metal to, say, 3/8" toss in the appropriate gears, grind a half assed 60° point and thread it to match the nut you found in the junk drawer. Your first threads don't need to be perfect, you'll learn far more by failing once or twice than you will by "nailing" it the first time every time. Once you have your first ones under your belt, improve on them. My point being; there is no better time than the one you are in...... 😎
Model Citizen
Well-Known Member
Oh Man, pink yo-yo’s are the dogs danglies ;-)

Golem,
The best one to sit down with you is you. You know what you want, you'll recognize it when you see and you'll always be your worst critic. Watch a video (I think Stuart de Haro has one) and have at it.
Also you need a **** it bucket, you're gonna screw up, it'll feel really good when the deposit rate drops.
Golem Pens
Michael
Mmmm yes and no. It's a learning style thing - some stuff I don't mind diving into, some things I definitely do better with instruction.The best one to sit down with you is you. Y
Mmmm yes and no. It's a learning style thing - some stuff I don't mind diving into, some things I definitely do better with instruction.
OK, have it your way. I think Air Canada flies direct to London Ontario. I'll pick you up there, flog you till you love single point threading, and give you room and board while you are here.
@jorogi's suggestion might be faster and is flog free.
Golem Pens
Michael
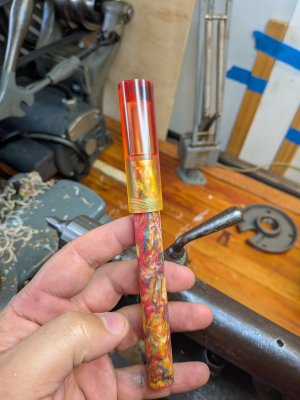
Needed a break from this stuff and had an idea for a different style of mandrel that seems to have worked out well. Nice big hogging pass here.

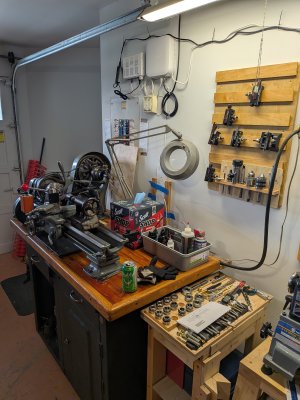
And finally got the new power cable management and general tidying of the area in hand. Feels better.
And finally got the new power cable management and general tidying of the area in hand. Feels better.
Attachments

Golem Pens
Michael
Thank you! This is the best this portion of the garage has felt in 7 months. Still some ongoing adjustments to make, especially re: tool storage, but it's proving to be pretty functionalSetup looks great!
Sadly, I'll never reach that point... 🙁...and then lock in on the little quality of life improvements
Golem Pens
Michael
The REST of the garage... is better not spoken about haha
Golem Pens
Michael
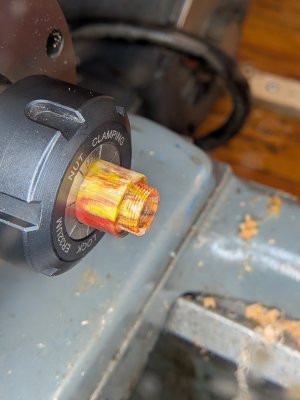
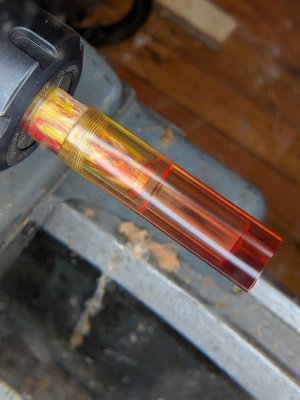
Decided to try boring the internal diameter (of the threaded portion) on this test piece and it really improves the internal/external concentricity (no duh, right?)
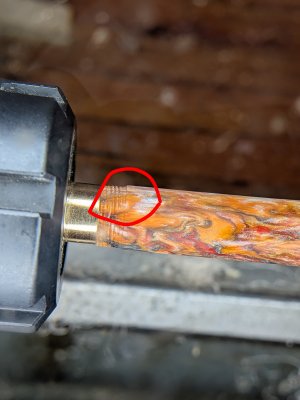
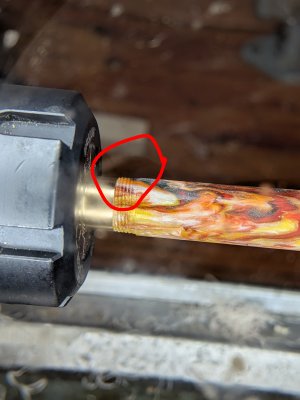
Now the debate of which way to hold the work for the external shaping. I've got a mandrel for both internal and external threads, they both have their pros and cons...
Now the debate of which way to hold the work for the external shaping. I've got a mandrel for both internal and external threads, they both have their pros and cons...
Attachments