• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

Dial reading shows travel, not depth of cut. So one thou on the dial reduces the work diameter by two thou.

Ah, I see. I wish mine was like yours. Mine reads diameter reduction. I am quite capable of calculating diameter change from a cut dimension. I want to dial in depth of cut not diameter.

All the other dials are travel. They should all be like that.

I think it's easier to internalize a diameter change from a depth of cut than the other way around. I would think that you will get the hang of it easier with the way yours works.
 
Oh yeah I'll get there with more hands on time, but right now I keep messing it up! (Doesn't help that my brain and schematics are still mostly in metric)
 
Oh yeah I'll get there with more hands on time, but right now I keep messing it up! (Doesn't help that my brain and schematics are still mostly in metric)

Consider making yourself or buying a metric/imperial conversion chart. Alternatively, I put a google home on the backsplash of my lathe. It can hear me at the mill or drill press or lathe. I can just ask it to convert anything to anything without changing pace.
 
My machine has a diameter reading dial in both metric and imperial….

The lead screws are imperial though with them being 10 tpi, the cross slide being 200 thou “diameter” removal per rev.

My old machine had what you have with the radius, and honestly, I preferred that. My brain thinks that way. The diameter removal confuses me.

But I’m not going to throw the baby out with the bathwater, just takes some getting used to.
 
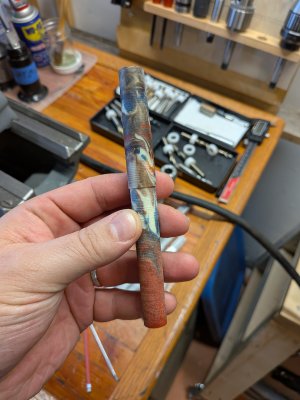
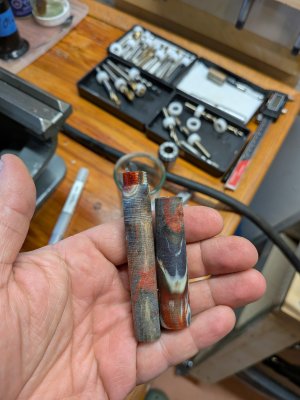
Not perfect concentricity on the tenon on this, but it's a lot better than before and I suspect this was user error (I didn't properly rounded the stock before mounting it in the collet and I think I moved it between operations).

At this point I would move to the wood lathe for some final manual shaping and then wet sanding.

Will give the last piece a go before trying a new one.
 

Attachments

  • PXL_20260120_221411473.jpg
    PXL_20260120_221411473.jpg
    1.4 MB · Views: 12
  • PXL_20260120_221433320.jpg
    PXL_20260120_221433320.jpg
    1.6 MB · Views: 12
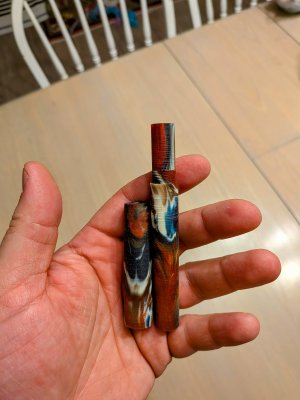
It's not bad, but still a liiiiittle more off concentric than I want. Obv needs final shaping and finishing. And I think I need to adjust my section drill bits - now that I have less runout some of the steps are too snug.

Overall, still very positive steps.
 

Attachments

  • PXL_20260121_023310854~2.jpg
    PXL_20260121_023310854~2.jpg
    1.6 MB · Views: 12
It's not bad, but still a liiiiittle more off concentric than I want. Obv needs final shaping and finishing. And I think I need to adjust my section drill bits - now that I have less runout some of the steps are too snug.

Overall, still very positive steps.
Looking good. Nice to be making stuff on the lathe instead of staring at it 😉

You’ll get better as you go along, all part of the fun!
 
Re made one of the pieces with more care to workflow (ie: actually trying the rod into round before turning any features), and I think the piece is looking quite nice, precision-wise.

However I decided to check my internal mandrels and all the ones I could use with this piece look out of whack. Tomorrow I'll see if they're maybe bent or can otherwise be brought closer to true...
 
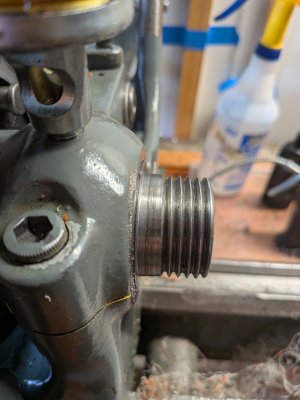
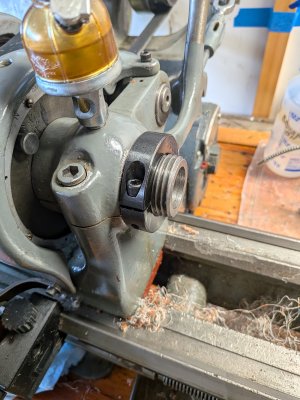
Latest shenanigans was turning down the really ugly chewed up bit of the spindle beside the shoulder. Now more like 1.5" so hopefully a decent 4 jaw chuck or backplate will be an option at some point (used that 1.5" ID collar just to test the fit, not really planning to use it). Just gotta find a suitable chuck 😉
 

Attachments

  • PXL_20260124_224059910.MACRO_FOCUS.jpg
    PXL_20260124_224059910.MACRO_FOCUS.jpg
    1.3 MB · Views: 10
  • PXL_20260124_224239984.jpg
    PXL_20260124_224239984.jpg
    1.8 MB · Views: 10
I'm eyeing this combination as a possibility.


Back
Top