• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

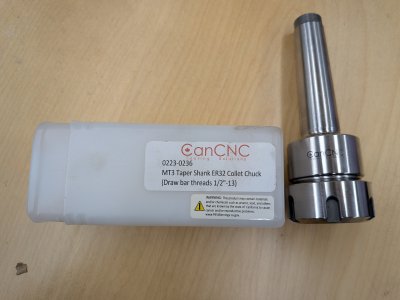
If you get a 4jaw situated and the mt3 er collet chuck

With the 3jaw you can always mount the backplate. Skim cut all the faces, then orientate the chuck thru all the mounting hole possibilities & you will likely find a combo that works as well.

Then when you fix the spindle with a press(or heat/cold) on bushing you will likely just need to reskim cut the 3jaw backplate.

No reason to give up on the lathe yet
 
You don't need to spend that kind of money to get a decent 4 jaw. Not only that but I think you can get a backplate included.

Are you looking for a 5"?

Did you ever sort out exactly what thread you need or are you going to go with an MT3 and drawbar?
I don't have a strong size preference honestly. At this point smaller is fine.

Thread is 1-1/2" x 8 TPI, confirmed.

Absolutely open to recommendations.

Right now MT3 and drawbar is lower on my list to explore.
 
I am out of 4 jaw chucks for sale, I am actually finally getting low on most everything. I need to assess my needs on my last two lathes before I over sell. I think I have already done that on one part. Lol.
However, I have another idea brewing........ I am pretty sure I have a spare 10k headstock that will have a good spindle, but I don't think I have a spare reverse tumbler....... enter @jcdammeyer and an els......... next problem is the tailstock will be 1/2" too low.... anyone local down for making a new lower shoe plate?
It's going to become a Franken-lathe but I don't think we're going to be hurting the resale value on a 9c....
I am on the island again this week and should be able to get the belt guard down to Victoria, but won't have much time to do much more than drop and run close to VIH or along the highway between Ladysmith and Victoria.
 
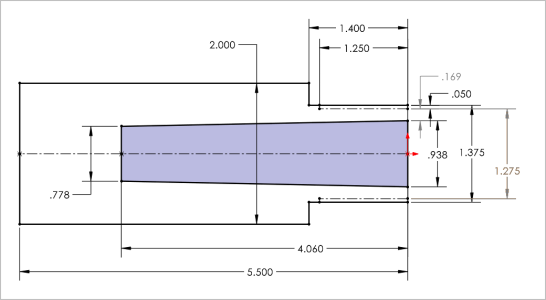
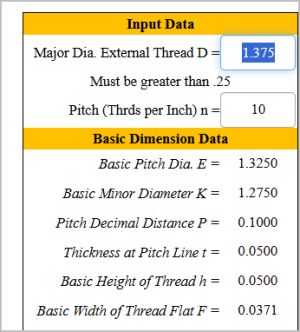
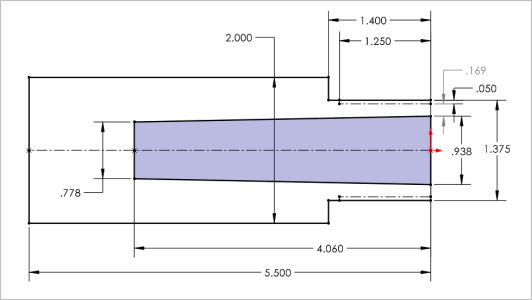
You can correct your actual dimensions & I can update, but just to give you a visual as I understand now, 1.375x10TPI thread yields 0.050" depth of thread. So you have about 0.169" of wall thickness to work with shaving the threads completely off

1768334094268.png1768334056163.png

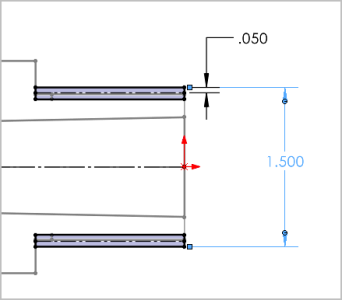
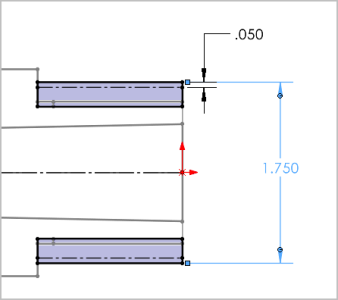
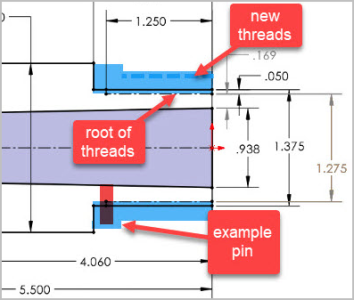
If you shaved the threads off to root bottom, new sleeves could look like this. 1.50 OD & 1.75 OD same TPI. Bigger would be better but I'm not sure what are common lathe back threads.
How it would be glued/pinned TBD. If you found a reputable shop/service, this might be a way to go. And this would simultaneously solve the vertical register issue because it would be turned in-situ at the same time. As mentioned it would be nice to have a donor spindle in case it didn't work. All you need is the length & bearing diameters to be a good match. Might even get one with a better non mangled MT bore which would solve the other problem.
1768334358800.png1768334385118.png
 

Attachments

  • 1768333949850.png
    1768333949850.png
    31.5 KB · Views: 0
Good idea on the 10K complete headstock,140mower.
The shoe for the tailstock would not be too hard to make.
Isn’t the F/R tumbler the same on 9 & 10K? I think so but i could be wrong.
Susquatch is right on buying a cheaper 4jaw. Usually need a back plate too.
Think 5” is good size, as new 4jaw chucks are lots heavier than old 4 jaws.
The tumblers are different, but I think modifications could be made, however.
I might be wrong, but I think an els would solve most all threading and powerfeed issues... I am pretty old skool, but I think @Golem Pens is young enough yet to not be as set in his ways, like some of us old dogs..... 😎
 
You can correct your actual dimensions & I can update, but just to give you a visual as I understand now, 1.375x10TPI thread yields 0.050" depth of thread. So you have about 0.169" of wall thickness to work with shaving the threads completely off

View attachment 76436View attachment 76435

If you shaved the threads off to root bottom, new sleeves could look like this. 1.50 OD & 1.75 OD same TPI. Bigger would be better but I'm not sure what are common lathe back threads.
How it would be glued/pinned TBD. If you found a reputable shop/service, this might be a way to go. And this would simultaneously solve the vertical register issue because it would be turned in-situ at the same time. As mentioned it would be nice to have a donor spindle in case it didn't work. All you need is the length & bearing diameters to be a good match. Might even get one with a better non mangled MT bore which would solve the other problem.
View attachment 76438View attachment 76439
Not sure if I'm reading you right but if you turn to the bottom of the threads depth and sleeving then when you cut the new threads you would end up with a spring. You'd have to cut deeper initially or use the bigger sleeve. Cut deeper, weaker spindle, thicker sleeve, possible issue with oddball back plate dimensions.
 
K
The tumblers are different, but I think modifications could be made, however.
I might be wrong, but I think an els would solve most all threading and powerfeed issues... I am pretty old skool, but I think @Golem Pens is young enough yet to not be as set in his ways, like some of us old dogs..... 😎
I was hoping to fit @jcdammeyer ELS system... After I got the dang thing operating manually.
 
Not sure if I'm reading you right but if you turn to the bottom of the threads depth and sleeving then when you cut the new threads you would end up with a spring. You'd have to cut deeper initially or use the bigger sleeve. Cut deeper, weaker spindle, thicker sleeve, possible issue with oddball back plate dimensions.
In both the sleeve sketches I'm showing resultant dimensions of an increased OD sleeve. I'm not sure if that's a good solution but just showing dimensionally what a sleeve would look like. His existing 1.375" has 0.169 of wall thickness from base of thread to ID of MT hole. That is not being reduced beyond existing thread root diameter. The threads above root diameter are not doing much if anything to resist torque. I would envision the sleeve being cross pinned into the spindle rather than relying on glue.
 
Back
Top