
-
Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
-
The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.
You are using an out of date browser. It may not display this or other websites correctly.
You should upgrade or use an alternative browser.
You should upgrade or use an alternative browser.
Working on my South Bend 9C
- Thread starter Golem Pens
- Start date

The post # 630 by @gerritv has measurements, this shows a spindle with a shoulder, however, the 1;5 X8 spindle nose is somewhat universal I think. It appears to show a thread length of 11/16 inch, a length of 7/8 inch from end of spindle to shoulder. I say appears as my eyes are still not over the pink eye bout.
These measurements could be confirmed by the other spindle. Have you tried the other spindle in your 3 jaw chuck mounting plate to check fit?
As @BaronJ has also said a bushing could be made for the “new” spindle. There was a picture of 2 pieces of bronze? stock shown in post #500 with a spindle, could the larger piece make a bushing?
Last edited:
I think I still got a can of that purple pink eye spray for the cows around here somewhere. Want I should make a flying trip up this afternoon?...my eyes are still not over the pink eye bout.
Thanks @JustaDB, it seems that a cold can be a carrier for pink eye, but pink eye comes in 2 flavours, a virus or a bacterial infection, I look LOL, barely, to have the viral one. So a waiting game— 7 days, as one eye got it about 2 days after the first one, about 9-10 days.
Anyway don’t want others to get this Kurap, and I would have SEE to round up some good beer. Gee, I have some gluten free stuff you could try, NOT, don’t know who thought it was beer, but I was stupid enough to buy it. Going to see if it will clean the drain in a while!
Anyway, thanks ,but another day. Though, I remember the livestock not liking that spray very much.

Golem Pens
Michael
Certainly could be!Hmmmmm.... Maybe someday (not now) that would be a good upgrade for your lathe....... The hardest thing to find is probably the spindle and you have that!
While I love a learning experience, I just want to get this dang thing running!

If there is no collar then what prevents the thrust to the left. Are there some sort of thrust bearings on the other end?Oh yeah... It's not compatible. I believe it's a more recent style than my lathe needs. The OD is smaller and I believe is intended for use with the generation that uses bronze press-in bearings (mine rides directly in the headstock).
Golem Pens
Michael
There are, yes. I'll grab a photo later, but basically from left to right the full assembly is...If there is no collar then what prevents the thrust to the left. Are there some sort of thrust bearings on the other end?
End with change gear > lock nut > left headstock > thrust bearing > spindle cone > bull gear > right headstock > spindle nose
Golem Pens
Michael
.... A shocking discovery via Facebook groups. Could it possibly be a 1-3/8"x10 ? Because this looks identical https://www.ebay.ca/itm/167284956776
Golem Pens
Michael
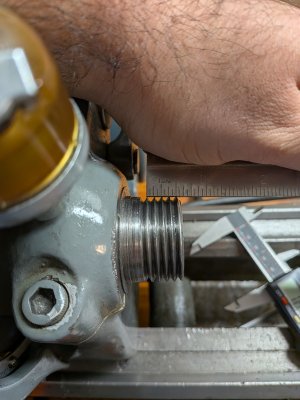

Well it looks like 10 tpi, but 1.5" OD. If I'm reading right.
Am I misunderstanding? Have you discovered that it's really 10 tpi, not 8? This would explain a shit load of runout....
A threaded connection is supposed to ramp a significant number of 60 degree threads against each other. The 60 degree cone surfaces self align as tension builds. The register forces a final alignment. But the register prolly couldn't fix an incorrectly matched sequence of threads.
Golem Pens
Michael
Disregard for now. Possibly but I don't trust my measurements so I'm picking up a new thread pitch gauge.Am I misunderstanding? Have you discovered that it's really 10 tpi, not 8? This would explain a shit load of runout....
A threaded connection is supposed to ramp a significant number of 60 degree threads against each other. The 60 degree cone surfaces self align as tension builds. The register forces a final alignment. But the register prolly couldn't fix an incorrectly matched sequence of threads.
Based off what I have now found elsewhere though it is a possibility.
Disregard for now. Possibly but I don't trust my measurements so I'm picking up a new thread pitch gauge.
Based off what I have now found elsewhere though it is a possibility.
I see! Thread gauges are not always that great. You can't go wrong just measuring them. A Vernier from point to point or valley to valley over as many threads as you have and some simple math will often be much better than a thread gauge. Just remember that you have count intervals not points. That seems to be a frequently made error.
Golem Pens
Michael
Yeah I counted 5 points to a half inch and then remembered that which is why I said disregard until I reconfirm hahahI see! Thread gauges are not always that great. You can't go wrong just measuring them. A Vernier from point to point or valley to valley over as many threads as you have and some simple math will often be much better than a thread gauge. Just remember that you have count intervals not points. That seems to be a frequently made error.
Yep. Hated it. But, like Buckley's Mixture, it just worked. 😉Though, I remember the livestock not liking that spray very much.
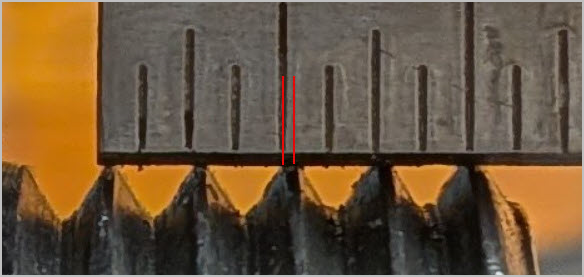
Yes use a caliper & encompass as many threads as you can. Photo parallax can be deceiving but something looks fishy. You can use this calculator to generate all the specs for ACME thread, OD, PD... by various class of fit. It says Fc = 0.0463" Just eyeballing yours maybe 25% of 1/16" rule increment = 0.016" ie. very sharp. Hard to image it could ever get worn like a leadscrew, <gulp> re-cut maybe? If the actual part is something other than an ACME you should be able to replicate with an online tool. Measure PD while you are investigating, easy to do with a mic & 3 wires.
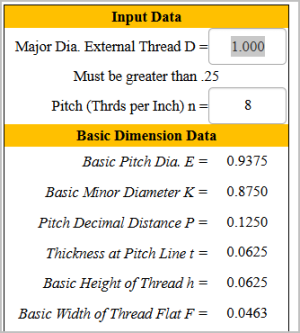
ACME General Purpose Thread Design Calculator
This ACME Thread General Purpose Design Calculator will determine the three classes of General Purpose, 2G, 3G, and 4G, for the external and internal threads.
www.engineersedge.com
Golem Pens
Michael
More archeology....
Early models did use 1-3/8"x10tpi at my bearing dimensions.
Later models settled on 1-1/2"x8tpi at the smaller diameter bearings.
And there is some documentation of transitional variants using the larger bearing and 1-1/2"x8tpi combination. A very odd duck, and likely not going to find a replacement.
The bearing diameter difference is about 0.025". Otherwise the "modern" spindle is the same length and everything else as my current one.
What does the bore look like on the threaded end? I just cant see welding working out without a lot of heat related distortion issues, but I have zero experience. I think you would stand a better chance of machining the threads off or nearly so to make a new surface, add a 'new' oversize collar & re-cutting the surface to spec or desired thread. The collar method has downsides too but its mechanically cold. I suspect you could get away with radial cross pins & strong bearing retainer for good measure. But how hard is the spindle core? Another question is how much meat is left given the spindle bore/socket ID? Of course this would have to be done on another lathe by someone that knows what they are doing. Maybe a 'somewhat close' spindle could be the lucky organ donor? The spindle & its rotating assembly is the beating heart of a lathe.
Golem Pens
Michael
The bore is in somewhat poor shape, it's certainly be mucked with in the past. Cleaning up the outside and re-extending the register surface with a collar seems.... Plausible.What does the bore look like on the threaded end? I just cant see welding working out without a lot of heat related distortion issues, but I have zero experience. I think you would stand a better chance of machining the threads off or nearly so to make a new surface, add a 'new' oversize collar & re-cutting the surface to spec or desired thread. The collar method has downsides too but its mechanically cold. I suspect you could get away with radial cross pins & strong bearing retainer for good measure. But how hard is the spindle core? Another question is how much meat is left given the spindle bore/socket ID? Of course this would have to be done on another lathe by someone that knows what they are doing. Maybe a 'somewhat close' spindle could be the lucky organ donor? The spindle & its rotating assembly is the beating heart of a lathe.