
-
Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
You are using an out of date browser. It may not display this or other websites correctly.
You should upgrade or use an alternative browser.
You should upgrade or use an alternative browser.
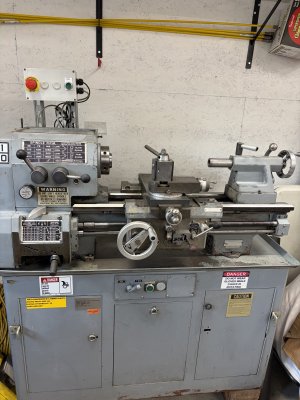
Standard-Modern lathe
- Thread starter Tahoetom
- Start date

slow-poke
Ultra Member
Nice lathe.
I have those parts, however I don’t want to part with them. I upgraded to ball screws however I always keep all the original parts. It would not be all that tricky to make a new parts assuming you have the old damaged parts.
If you don’t mind sharing, how much did you pay for your lathe, and where did you source it?
I have those parts, however I don’t want to part with them. I upgraded to ball screws however I always keep all the original parts. It would not be all that tricky to make a new parts assuming you have the old damaged parts.
If you don’t mind sharing, how much did you pay for your lathe, and where did you source it?
slow-poke
Ultra Member
Not too difficult , but I decided to go one size up instead of one size down compared to the original so getting the nut squeezed in there was somewhat challenging. If doing it again, I would go one size down it would be a lot easier. The problem for you would be the difference in thread pitch, that would throw off your dial graduations. That was not an issue for me because of CNC conversion.Was it difficult to change to ball screws
Sure beats winning the fuzzy dice at the draw
Thanks for the info, dro will fix the dial issue I guess. I’ll look into it.Not too difficult , but I decided to go one size up instead of one size down compared to the original so getting the nut squeezed in there was somewhat challenging. If doing it again, I would go one size down it would be a lot easier. The problem for you would be the difference in thread pitch, that would throw off your dial graduations. That was not an issue for me because of CNC conversion.
Sure beats winning the fuzzy dice at the draw

140mower
Don
Someone wiser than me will be along shortly, but I think from what I have heard you'll need to have a way of locking the cross slide as there's not enough friction in the ball and screw to hold position while taking a cut. In a cnc, the servos take care of that.Thanks for the info, dro will fix the dial issue I guess. I’ll look into it.

skippyelwell
Ultra Member
Did you take any photos of the change over?Not too difficult , but I decided to go one size up instead of one size down compared to the original so getting the nut squeezed in there was somewhat challenging. If doing it again, I would go one size down it would be a lot easier. The problem for you would be the difference in thread pitch, that would throw off your dial graduations. That was not an issue for me because of CNC conversion.
slow-poke
Ultra Member
Did you take any photos of the change over?
I should have, but don’t think I did. I will check.
The cross slide just takes a few minutes to remove and once you flip it over on the bench everything is easy to access. The slot for the nut is fairly narrow and is a raw casting so the width of the slot was not perfectly consistent. I cleaned up the squareness of the slot with a Dremil tool. I should have thrown it on the mill (would have been faster/better). There is a lot of material to the sides, that I could have machined wider but I didn’t want to compromise the rigidity. When doing CNC conversions I prefer to not machine any of the original cast iron to allow a complete restoration to original if desired in the future. So far on the four conversions, I have only had to drill and tap a few mounting holes.
Only because I upsized, the mounting block for the nut was really tight, I ended up grinding most of the flange portion of the nut off and then the top portion that accepts the mounting bolt from above had just enough material. If I had down sized, there would have been more room; top and either side.
One other thing, the original lead screw is left hand thread, while the generic (read cheap), ball screw is right hand thread, which is irrelevant when driving with a servo.
Last edited:
Lightspeed Mike
Super User
I have a Standard modern lathe too. The cross screw was worn out on mine. It was a 9/16" left hand acme thread. Unable to source a length of that threaded rod I had a local machine shop make one for me.
Lightspeed Mike
Super User
It was a couple of years ago, but I thank only about $250.I hate the fact that I have to source a part that I could easily make if I had access to a lathe and mill. I hate to ask what they charged you for it
They did a really nice job. My machining capabilities were definitely not up to what they needed to be to make it.
I priced out a new cross screw from Standard Modern to the price of over $1000. 😵

The real milo
New Member
Congratulations on winning that lathe in the draw. Finding original Standard Modern parts for a 10x20 is difficult today because they have been out of production for decades although vintage Canadian machinery dealers like Plaza Machinery occasionally stock parts machines. If you still have the damaged screw to measure the thread pitch and bearing journals your most reliable option is purchasing matching Acme threaded rod and bronze nut stock from McMaster Carr or Roton. You can then machine the plain journal ends to match the original dimensions or ask a local shop to turn them. Any standard keyed handwheel from KBC Tools will fit the handle.I’ve recently acquired a 10x20 Standard-Modern lathe which requires a few parts, namely a cross feed screw and handle. Having trouble sourcing parts. Anyone have any parts or leads?
Thanks