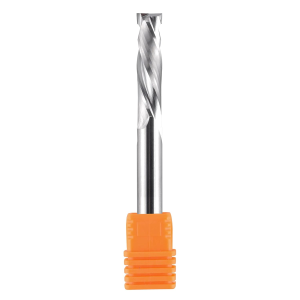
Just to be clear here too the Machinist Workshop of course expecting that I have a $100K US HAAS and need to turn out 2,000 parts per hour comes up with these incredible values for 6061 Al and this is for a finishing pass.
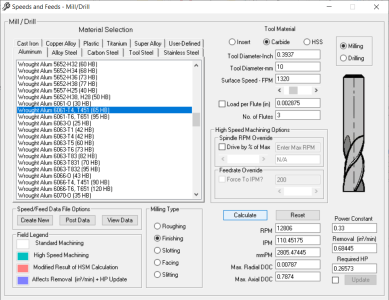
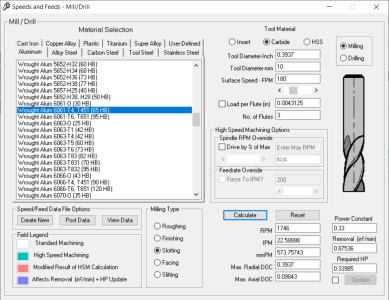
Seriously although I can effortlessly do 110 IPM the 12,806 RPM is almost 4.5x the amount I can spin my tool bit. So instead I cut down the Surface Speed FPM to 180 and get more reasonable values.
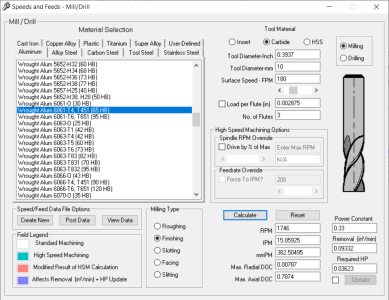
But I'm assuming this would still be with full 3 nozzle flood coolant? After all this part is only 14mm thick (0.551") so theoretically I could cut this out in one pass.
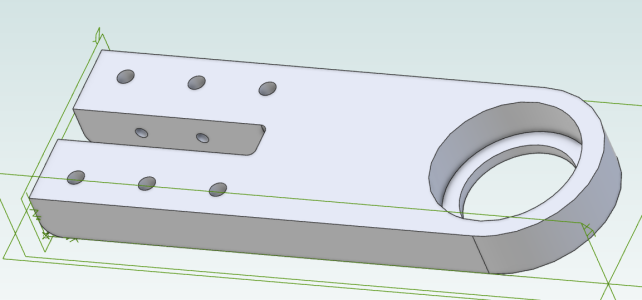
But that's way too optimistic right?
Say I am cutting this out of a larger piece of plate. Then it's really slotting isn't it? Now the axial depth of cut drops to 0.09843" or 2.5mm per pass.
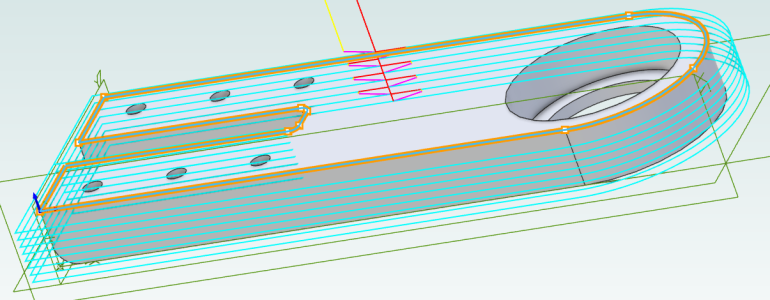
If I set it to 2mm per pass for example it looks like this with 8 passes and the last just a tiny bit to get past into the spoil board. This is with 0.05mm outside of the final dimension. Then just a full depth cleanup pass.
For an experienced machinist with a non-HAAS CNC mill what would you use for this?
Seriously although I can effortlessly do 110 IPM the 12,806 RPM is almost 4.5x the amount I can spin my tool bit. So instead I cut down the Surface Speed FPM to 180 and get more reasonable values.
But I'm assuming this would still be with full 3 nozzle flood coolant? After all this part is only 14mm thick (0.551") so theoretically I could cut this out in one pass.
But that's way too optimistic right?
Say I am cutting this out of a larger piece of plate. Then it's really slotting isn't it? Now the axial depth of cut drops to 0.09843" or 2.5mm per pass.
If I set it to 2mm per pass for example it looks like this with 8 passes and the last just a tiny bit to get past into the spoil board. This is with 0.05mm outside of the final dimension. Then just a full depth cleanup pass.
For an experienced machinist with a non-HAAS CNC mill what would you use for this?