• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.

JCDammeyer's 42 projects

Sh-t happens, I'm just glad you weren't in the way when it blew.
Yeah. That's what my wife said when she got home from work. Hanging on a hook in front of the regulator is the hose and a second longer hose to be able to get further out onto the driveway. So when it blew it likely just hit the hose and dropped down behind the MIG welder and oxy/acet. tanks. I'll look for it when I clean up around there.

But yes. Shrapnel is never a fun idea.
 
Ah yes, the mushrooms.
Was living in Oregon in early 70’s.
There was a large hay barn along Interstate 5 around Brownsville, years old hay left to rot.
For about a month students from Univ of Oregon & Oregon State were harvesting Magic Mushrooms until the state finally had to put a stop to it & dispose of hundreds of bales.
This was Ken Kesey’s neighborhood.
Good Times.
 
Hi Guys,

Quite a few years ago, I used to go to a farm with a shop and had a gate on the main road. They are still there 50 odd years later and still have the shop where I used to go to buy the mushrooms that they grew in the big hay barn. They were about 6 inches in diameter and my mum used to stuff them with cottage cheese, served with bacon and an egg !

We/I still go there to buy potting compost !
 
How's the eye doing John?
Not bad. Fixing the right lens from a different pair into the empty spot of the left at least gives me pseudo good vision.I can now take my glasses off and read the cell phone or a book if it's not too far away; with both eyes. At times vision is still somewhat distorted.

Two more weeks of drops and then I can get an eye exam and get some new lenses. I believe the cause of the rapid deterioration of the left was likely due to it becoming so hard it couldn't be flexed to focus. Hence the change from -6.5 to -7.5 to -8.75 in a 6 month period.

I can now see how the right eye is tinting everything a bit yellow. So I guess I just have to watch out for it and if it starts having focus problems get that one done too.

Even with the vision issues I am making progress on the robot arm.
 
SWMBO just went in to get new reading glasses, salesperson was desperate to convince her she needs blue blockers, ani-glare ratings, etc. Very young salesperson was shocked to discover that all that high-tech crap is factory-installed in the aftermarket lenses that SWMBO already has installed in her eyeballs.
 
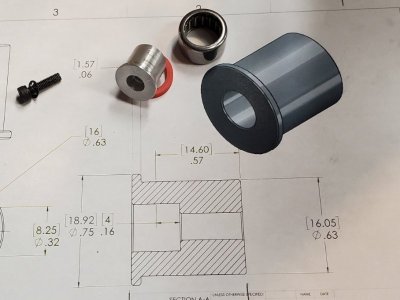
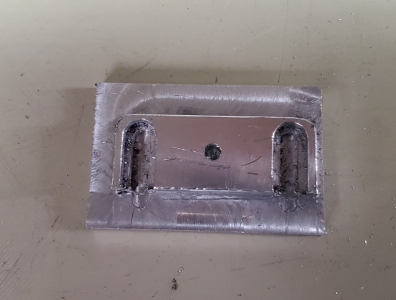
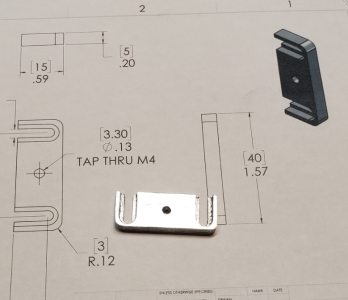
So a bit more work on the Robot Arm. The J5 Bearing post holds a needle bearing which serves as an idler and tension adjustment for the wrist joint. Turns out some of the dimensions are missing from the drawing. I measured the flange diameter which was listed as 0.75" and it matched the overall length so that's how I built it. Turns out that was wrong.

J5BearingPost.jpg

I had to shorten it by 2mm. Holding onto that part when there's a flange and removing 2mm from the back end was an interesting experience. I 3D printed the spacer with PETG as described for the AR4-MK4 arm project and then after cleaning it up screwed the works down onto the bracket I made and talked about in this thread.

J5_Mechanism-1.jpg

This week I'll be allowed to lift heavy stuff so I may just fire up the foundry to cast some of the pieces. Meanwhile I'm working on the electronics panel. More as it happens.
 
So a bit more work on the Robot Arm. The J5 Bearing post holds a needle bearing which serves as an idler and tension adjustment for the wrist joint. Turns out some of the dimensions are missing from the drawing. I measured the flange diameter which was listed as 0.75" and it matched the overall length so that's how I built it. Turns out that was wrong.

View attachment 78695

I had to shorten it by 2mm. Holding onto that part when there's a flange and removing 2mm from the back end was an interesting experience. I 3D printed the spacer with PETG as described for the AR4-MK4 arm project and then after cleaning it up screwed the works down onto the bracket I made and talked about in this thread.

View attachment 78696

This week I'll be allowed to lift heavy stuff so I may just fire up the foundry to cast some of the pieces. Meanwhile I'm working on the electronics panel. More as it happens.
Looking great, but please tell me you won't be pulling a "Wolowitz"..... 😱
 
Hi John, from another John.

I would have used a set of narrow soft jaws to hold that J5 ? with the flange behind the jaws. Then no danger of damaging the flange.
 
Hi John, from another John.

I would have used a set of narrow soft jaws to hold that J5 ? with the flange behind the jaws. Then no danger of damaging the flange.
If I had that I would have done that. Instead I used a long 4mm socket head screw with two nuts. I held the end of the screw in the 3 Jaw and then used the parting tool to cut on the line for the proper length.

It broke loose with a tiny bit of material which I was able to cut away with diagonal side cutters. Then just hand drill and chamfer bit. It was the correct length within about 0.02mm.

I must say, drilling the hole for the head of the socket screw to a precise depth is the first time I've wished for a scale on the tail stock.

Solution was to enlarge the hole with a 'P' size drill to almost the correct depth. Then a teensy boring cutter from my Unimat tool set. Setting the cutter to the surface as 0.000" and the END position to 0.240" on my ELS and then I had the ELS move the cutter as I bored the hole to the correct depth and dimension.

The whole thing took way longer than it does to tell the story. However the needle bearing fits perfectly. The PETG plastic spacer was a tad thick from the 3D printing but sanding it down until I had clearance wasn't a big deal.

I have learned so much about CAM and CNC doing this project. And still so much more to learn.
 
Hi John,
This is where making some to fit the chuck jaws comes in very handy. I don't have any ability to do 3D printing, but how long would it take to actually print a set ? It would probably take longer to thread them.
 
Hi John,
This is where making some to fit the chuck jaws comes in very handy. I don't have any ability to do 3D printing, but how long would it take to actually print a set ? It would probably take longer to thread them.
Hadn't thought of that. A few hours to design and print. But even just turning down a stub arbour would likely take less time. Or start off with the correct dimensions.

In this case, because I didn't have any 0.75" diameter aluminum stock instead I took an old sprue and carefully turned it down until it could be securely held in the 3-jaw. This was actually a nice piece of cast al. Turned very easily, no gumming. Biggest problems with using a sprue is they are tapered and the top has the wide area that flowed over the surface of the sand. Hard to hold in the vice to cut shorter.
 
Hi John,

I've got away with using a short length of thick wall plastic pipe to hold slightly tapered things in the lathe three jaw. You do have to be careful though, if its too tapered it tends to walk.
 
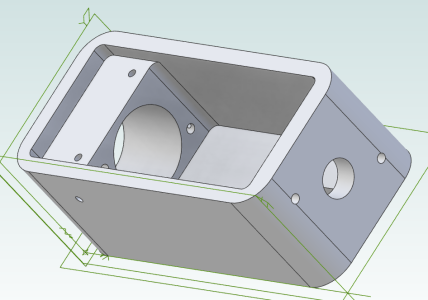
So I want to make this part.
1772058132991.png
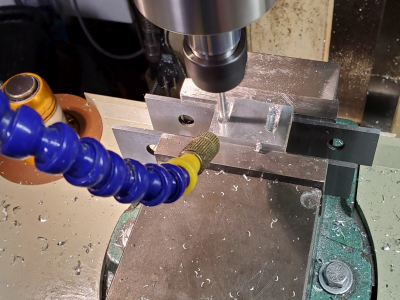
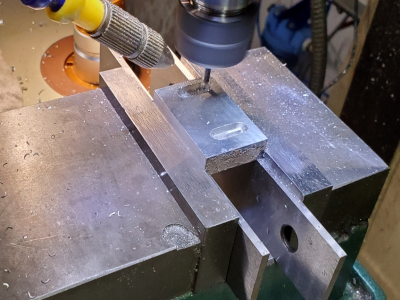
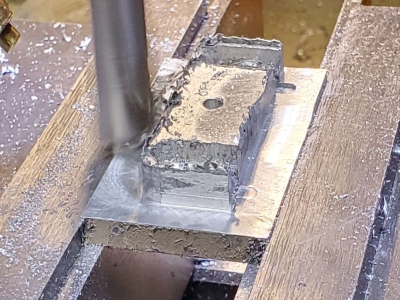
The milling depth is 35mm and I'll likely cast the basic block with most of the recess already there. Both these end mills look like they could do the job.

Opinions? Suggestions?

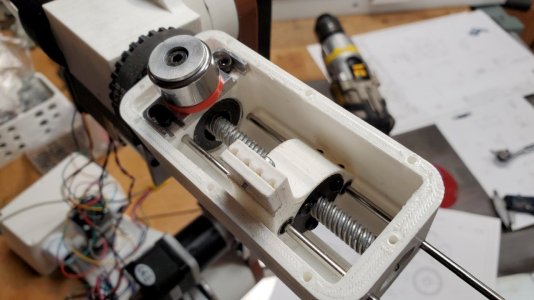
One of the key features of this part is that the two large holes and the small ones need to be precisely placed. The two small ones are guide rails for the part moved by the lead screw as shown in the picture a few postings back.

I think the bottom clamped to a right angle plate and the one side as a reference and then bored and drilled onto the end.
 
Last edited:
The biggest diameter you can use will help to reduce chatter, so 3/8". But also I would be looking at a carbide endmill, simply due to the increase in rigidity. North American suppliers of those will be very expensive, but an 8mm carbide will easily outperform a slightly larger 3/8" (9.5mm) HSS endmill - the carbide is 3x stiffer.
So a 8mm asian sourced endmill should be about the same cost as the KBC one after shipping, give or take $5-$10, unless you are already getting stuff from KBC or can walk there...
quick examples:
https://www.aliexpress.com/item/1005003179556695.html $37.58 shipping in
https://www.aliexpress.com/item/1005006117203437.html $37.31 ($31.99 + $5.32 shipping)
(I don't think the border people have figured out the T word on this stuff yet so there's that savings too, not that we all shouldn't pay our share, just nice to get small break once in a while.)

I rarely check the jungle store, but today they seem to have something that fits the bill even better than above - 3/8" carbide for less than the KBC HSS:
https://www.amazon.ca/Carbide-Cutting-Diameter-Stainless-Aluminum/dp/B0D12TFQL4 $30.99 minus $9.30 coupon = $21.69 seems worth giving a try. gets you full 3/8" diameter in Carbide and 1.375" flute depth. (basically 35mm).

 
The biggest diameter you can use will help to reduce chatter, so 3/8". But also I would be looking at a carbide endmill, simply due to the increase in rigidity. North American suppliers of those will be very expensive, but an 8mm carbide will easily outperform a slightly larger 3/8" (9.5mm) HSS endmill - the carbide is 3x stiffer.
So a 8mm asian sourced endmill should be about the same cost as the KBC one after shipping, give or take $5-$10, unless you are already getting stuff from KBC or can walk there...
quick examples:
https://www.aliexpress.com/item/1005003179556695.html $37.58 shipping in
https://www.aliexpress.com/item/1005006117203437.html $37.31 ($31.99 + $5.32 shipping)
(I don't think the border people have figured out the T word on this stuff yet so there's that savings too, not that we all shouldn't pay our share, just nice to get small break once in a while.)

I rarely check the jungle store, but today they seem to have something that fits the bill even better than above - 3/8" carbide for less than the KBC HSS:
https://www.amazon.ca/Carbide-Cutting-Diameter-Stainless-Aluminum/dp/B0D12TFQL4 $30.99 minus $9.30 coupon = $21.69 seems worth giving a try. gets you full 3/8" diameter in Carbide and 1.375" flute depth. (basically 35mm).
Thanks. I've ordered a 40mm since I also have one other part that is just on the edge of that. Plus since my imperial ER20 collets don't fit a 10mm (I have one of those but not long enough) I've also ordered an 8mm and 10mm ER20 collet.

It's always tools that drive the costs of everything. And that I tend to break the smaller ones...
 
The 3 Flute for Al. goes way up in price when they are longer. My D10x30x75 carbide 3 flute arrived last week but I don't have a collet to hold it. Silly me and the 30 is just a tad short for the box but will be great for the 1/2" plate I have her for stuff.

So I ordered a 2 flute D8x45x120 Carbide and also a 3 Flute D10x40x100 carbide. The D8 two flute was way more than the 3 flute but that's because it's just that tad longer.

Should work fine with cast aluminum.
 
Back
Top