
-
Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
You are using an out of date browser. It may not display this or other websites correctly.
You should upgrade or use an alternative browser.
You should upgrade or use an alternative browser.
JCDammeyer's 42 projects
- Thread starter jcdammeyer
- Start date

I don't get it.Is this the new face of machining ?
Oh goody 🙄

Wrapping my head around the differences in our mills; your spindle is stationary and the knee moves up vs my stationary table and moving spindle.In my case between re-probing etc. I'm still off by as much as 0.005" when I measure things. I think the backlash in the Z axis, even with compensation is screwing things up.
How can the Z backlash be a factor when all the measurement occurs when the backlash has taken out as a result of the knee moving up?
Yes. And the people that wrote the code also have a machine where the head moved so some of the explanations were also confusing.Wrapping my head around the differences in our mills; your spindle is stationary and the knee moves up vs my stationary table and moving spindle.
How can the Z backlash be a factor when all the measurement occurs when the backlash has taken out as a result of the knee moving up?
Recall posting https://canadianhobbymetalworkers.com/threads/jcdammeyers-42-projects.9677/post-217560
That bevel gear once loaded shouldn't have backlash. However I think for probing I might not have moved up and down enough to properly remove that.
Another thing I noticed this evening is the speed with which the backlash is removed. When you are milling a profile and the axis has to change direction it needs to happen immediately and quickly in order to meet the criteria for milling a smooth curve.
I noticed this evening that the speed to change direction on Z makes (or can make) quite the bang on the bevel gears.
Tonight I cleaned the mill table, bottom of the vise and use the 'good' parallels. Touched off with the probe. Pretended the 1/2" HSS 4 flute cutter end mill didn't have a length measurement so it had to be measured on the tool setter.
This time I had to crank the knee up 0.005" before chips came off. Set that as my zero point and then depth of cut.
Milled a nice smooth surface taking 0.005" at 2800 RPM. Picture doesn't do it justice. Super smooth and parallel at least measured with the calipers. Maybe less than 0.0005" (0.012mm) difference over the length and that's more likely my vise.
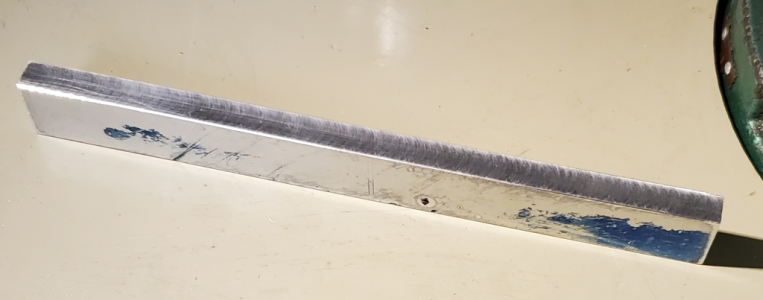
Next project for this mill has to be a ball screw on the knee.
Learned a lot.
Thanks. I'm still going to finish my longer document with photos and drawings. To make sure I really do understand. I'll get you to proof read it.
Happy to!Thanks. I'm still going to finish my longer document with photos and drawings. To make sure I really do understand. I'll get you to proof read it.
Sorry John, just the cynical luddite in me. I am truly impressed with the power of CNC but the journey to get there would hurt so much. Ironically 50 or so years ago I was the kid who spent hours at the punch card machine, then would jump on the bus, ride across town to UVIC, put the cards in the inbox and wait for operator to run the program and put my cards and printout in my box. Inevitably my results would be "syntax error at line 54". Get home by 22:00 and have another whack at it again next day.I don't get it.
I am determinedly trying to ignore all this AI stuff being crammed into my face. In the last two days I decided to ask it two simple questions and both times the answers were completely wrong. And the kids just lap it up.
Sorry, rant over.
Gawd I remember those punch card days.Sorry John, just the cynical luddite in me. I am truly impressed with the power of CNC but the journey to get there would hurt so much. Ironically 50 or so years ago I was the kid who spent hours at the punch card machine, then would jump on the bus, ride across town to UVIC, put the cards in the inbox and wait for operator to run the program and put my cards and printout in my box. Inevitably my results would be "syntax error at line 54". Get home by 22:00 and have another whack at it again next day.
I am determinedly trying to ignore all this AI stuff being crammed into my face. In the last two days I decided to ask it two simple questions and both times the answers were completely wrong. And the kids just lap it up.
Sorry, rant over.
And I'm someone who doesn't want to upgrade to WIN-11. Don't really want to upgrade a lot of my software. Works just fine.
My first exposure to Unix was on a PDP-10. Graphics software for analyzing satellite maps for a Grad Level Course.
Still don't like a command line oriented programming world.
Much of how I use my mill could be just as easily done with something more like my ELS but with all three axis.
The real problem in the CNC world right now is too many flavours. Add the CNC routers to the mix and use one of those where the router goes up and down and use a knee mill where the spindle doesn't move and all motion is backwards.
Enough to convince me to take up knitting...
I'm thinking of building a knitting machine...Gawd I remember those punch card days.
And I'm someone who doesn't want to upgrade to WIN-11. Don't really want to upgrade a lot of my software. Works just fine.
My first exposure to Unix was on a PDP-10. Graphics software for analyzing satellite maps for a Grad Level Course.
Still don't like a command line oriented programming world.
Much of how I use my mill could be just as easily done with something more like my ELS but with all three axis.
The real problem in the CNC world right now is too many flavours. Add the CNC routers to the mix and use one of those where the router goes up and down and use a knee mill where the spindle doesn't move and all motion is backwards.
Enough to convince me to take up knitting...
Can you afford the time? Knit one, then a bunch of oysters to farm for pearl two. Or something like that...I'm thinking of building a knitting machine...

slow-poke
Ultra Member
Well worth the effort.Next project for this mill has to be a ball screw on the knee.
I initially thought that the knee would be the most challenging, but in a way it's easier because you don't need to remove the tables to get access to the nut/screw.
I find more and more often I start doing a simple task for example yesterday I was drilling a bunch of holes. I had the locations mapped out and planned to just use the quill for the actual drilling. After a couple of holes I thought what am I doing? A few lines of code later and the holes were getting drillied while I watched. Lets me do something else while the work is getting done.
It's a bit like having a free junior employee except they work 24/7 and our very consistent. That being said if I'm not careful coding it will behave with "attitude".

Sorry John, just the cynical luddite in me. I am truly impressed with the power of CNC but the journey to get there would hurt so much. Ironically 50 or so years ago I was the kid who spent hours at the punch card machine, then would jump on the bus, ride across town to UVIC, put the cards in the inbox and wait for operator to run the program and put my cards and printout in my box.
Gawd I remember those punch card days. And I'm someone who doesn't want to upgrade to WIN-11. Don't really want to upgrade a lot of my software. Works just fine.
I don't think that's being a luddite. I too remember punch cards. What a drag. Sometime a few years later, I started programming the 4040 in machine language (it had no assembler yet). You just wrote your program out in long form and then added it to memory one binary code step at a time. Then I moved to an 8080. When an assembler for the 8080 arrived, I thought I had died and gone to heaven.
I just upgraded 2 laptops and a desktop to Windows 11 last week. Holy crap..... Soooooo many problems. One desktop isn't compatible so there is that challenge yet to face.
But CNC machining? Not for me either @jorogi. I helped bring robots to the auto industry. If I had to make one identical part every 50 seconds, I'd be all over CNC. But that isn't what I do. I make one part maybe two. Then on to something else. Manual machining is perfect for me. I enjoy turning hand cranks, feeling the cutter feedback, and making it happy.
I like following what you CNC guys are doing, but I'm happy cranking handles manually for my own work. I don't feel like a luddite - I feel like an artist freed from the horror of an automated factory churning out identical parts. I am making stuff with my own two hands surrounded by birds and wildlife and watching things grow. It is blissful, peaceful, and idyllic. A great way to live out my final years.
Now 3D Printing? That's in my future! Just need to figure out how to convince the lady that we need it, or how to hide it till I die.

Doggggboy
Ultra Member
Which would be only a few brief moments after she found it?Just need to figure out how to convince the lady that we need it, or how to hide it till I die.
I find I do use the MDI a lot. For example to surface that scrap piece for testing I set up where XYZ Home was and entered inWell worth the effort.
I initially thought that the knee would be the most challenging, but in a way it's easier because you don't need to remove the tables to get access to the nut/screw.
I find more and more often I start doing a simple task for example yesterday I was drilling a bunch of holes. I had the locations mapped out and planned to just use the quill for the actual drilling. After a couple of holes I thought what am I doing? A few lines of code later and the holes were getting drillied while I watched. Lets me do something else while the work is getting done.
It's a bit like having a free junior employee except they work 24/7 and our very consistent. That being said if I'm not careful coding it will behave with "attitude".
T99 M6 G43 which loads my probe. Press the button to move it to XY home which is outside the part. Then down within about .25" of the top surface with the MPG or jog buttons and run Touch Off top Surface.
Then T05 M6 G43 to load and measure the 1/2" end mill.
Again click on the goto XY home and then goto Z home buttons. If all went well the cutter should just scratch the surface. I jog over and using the MPG move it between 0.001 and 0.005 to reach the surface.
Press button to go back to XY == 0 and then use MPG to move Z to depth of cut.
S2500 M3 to switch on the spindle,
G1 X8 F10 to mill to the end.
G1 X0 F10 to return.
M5 to switch off Spindle or press STOP on MPG pendant.
After that it's a matter of setting a new depth and pulling the commands off the history list. If the surfacing had to do several passes I might just copy and paste those commands into a text file saved as something.ngc. Load it and run it.
Yeah... I now have two and a failed Delta 3D. And now the 3:1 sheet metal bender/sheer/roller sits mostly unused as does the corner notcher and a few other tools. Those were bought with the intention of making boxes for electronic projects. But instead 3D printing took over.Which would be only a few brief moments after she found it?
In either case though, without CAD both approaches are useless.
Elektrishun
Ultra Member
Now 3D Printing? That's in my future! Just need to figure out how to convince the lady that we need it, or how to hide it till I die.
Find a way to bridge the gap. She says, "This plastic handle broke. These are so old...where will we ever find one to match?" That's where you speak up and say, "If I had a 3D printer..."
A 3D printer is on my tool bucket list, too. Did the deep research dive a few times on 3D printers but haven't pulled the trigger yet.
Find a way to bridge the gap. She says, "This plastic handle broke. These are so old...where will we ever find one to match?" That's where you speak up and say, "If I had a 3D printer..."
I've already tried that. She just starts spouting dollars and cents. She is like that. I am pretty sure it's gunna take a $5000 ceramic tile floor in the kitchen and backroom.
Did the deep research dive a few times on 3D printers but haven't pulled the trigger yet.
Exactly where I am. Keep hoping a new model will do everything, be bug free, plug N play, and cost under 200. That I could swing.
Bambu A1 mini.Exactly where I am. Keep hoping a new model will do everything (small), be bug free, plug N play, and cost under 200. That I could swing.
Bambu A1 mini.
Ya right, small wasn't (and isn't) in my requirements......