
Fergusmacfurkin
Member
As mentioned in my intro a month or two ago, I bought a lathe because I need to manufacture some parts for a Saxophone restoration I'm working on and the parts haven't been manufactured since the 60s. Why do I do this to myself?
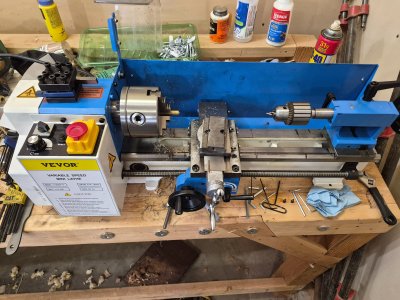
Anyway, after many hours of tweaking, cleaning, praying and quiet cursing I have managed to get first chips off my vevor mini lathe. So far, it's.... functional.
First, the good:
- I was able to face down the plastic sanding block I needed for leveling the tone holes. So, one tool made. will probably need to to a few more for the smaller holes as I go.
- It was able to handle the piece of 3/4 round 4140 I threw at it if I took light passes and produced a decent surface finish all things considered. So, step one of the crimping dies is complete and I have a *fairly* central center drill mark for reference.
- The tail stock has the same taper as my wood lathe, so I can use my jacobs chuck from that. (more on that later)
- Was getting some nice chips and spirals off the 4140, though that is more on the cutter than me.
The not-so-good:
- In spite of all my efforts and copious amounts of lubrication, the feeds still bind and are stiff. I'm going to need to disassemble everything again at some point and put a straight edge on the dovetails and gib. Probably going to need a new gib. Is using brass for that a good idea or bad? It'll be hand made job, so brass would be A LOT easier to do. I might even be able to score some bearing bronze from work... we'll see.
- The tail stock is as rigid as a wet noodle. It would probably suffice for tail support, and the dead center that came with it is probably functional enough. It has a short morse taper on it so the tail stock doesn't have to extend three miles out to engage it. My jacobs chuck from the wood lathe..... it's almost at full extension and the rigidity leave a lot to be desired. not even sure of the alignment, TBH. But that is something I will address once it has a permanent home and is bolted to something solid.
- The handles on the cross feed and compound feed have a habit of unscrewing themselves. Nothing some loctite or turning a new handle won't fix, but annoying. (possibly a safety thing, now that I think on it. Really don't want my hands slipping near a chuck)
- getting the chuck jaws to come together evenly when swapping is a bit fiddly. pretty sure that's user error though.
The OH FOR F'S SAKE!!!!:
- The tool post is too high. I'm using 3/8 braised carbide tools for now until I get the grinder set up and can start grinding my own HSS tooling. (Got the blanks just need to grind them.) and my first first facing pass on the 4140 stalled out and started rubbing almost half a millimeter out from center. (yes, I checked against the dead center on the tailstock and even tried the ruler trick) took it out and filed down the underside. tried again, ruler trick said it should be fine.... nope. Now, in fairness to the lathe, I don't doubt that 4140 surface hardened on me when it started rubbing and many of my trouble stem from that. So I grabbed my mic and checked how thick the bit was..... it's has the thinnest body in the kit.... balls! I didn't think to check the cutter height as compared to the body.. need to check that. Either way... this is a problem and maybe it's one of my own creation. Input is welcome. I'm planning on getting a quick change tool post so that should alleviate the pain a bit.
- There are no gradations on the main feed. It's just a black hand wheel... future project.
Suggestions needed:
- bronze/brass gib: good idea? bad idea?
- is there anything special that bronze needs for being worked? How prone to work hardening is it? Any traps to avoid while annealing? my experience working with bronze mainly involves a carbide burr on a die grinder or throwing it in liquid nitrogen before stuffing it in a hole.
- preferences for shim stock for shimming tools in the tool post? I have brass shim stock or am I better off buying some sacrificial feeler gauges from princess auto?
- any thoughts on lowering the toolpost? Is there a place in the carriage that I should look or am I looking at having to file down the bottom of the holder to lower tool height since it seems to be across multiple cutters? Should I be looking at retooling in 5/16 unit I replace it with a quick change post? I'm leaning to retooling, but I really don't want to. I'd rather that cash went towards the better tool post.
Anyway, after many hours of tweaking, cleaning, praying and quiet cursing I have managed to get first chips off my vevor mini lathe. So far, it's.... functional.
First, the good:
- I was able to face down the plastic sanding block I needed for leveling the tone holes. So, one tool made. will probably need to to a few more for the smaller holes as I go.
- It was able to handle the piece of 3/4 round 4140 I threw at it if I took light passes and produced a decent surface finish all things considered. So, step one of the crimping dies is complete and I have a *fairly* central center drill mark for reference.
- The tail stock has the same taper as my wood lathe, so I can use my jacobs chuck from that. (more on that later)
- Was getting some nice chips and spirals off the 4140, though that is more on the cutter than me.
The not-so-good:
- In spite of all my efforts and copious amounts of lubrication, the feeds still bind and are stiff. I'm going to need to disassemble everything again at some point and put a straight edge on the dovetails and gib. Probably going to need a new gib. Is using brass for that a good idea or bad? It'll be hand made job, so brass would be A LOT easier to do. I might even be able to score some bearing bronze from work... we'll see.
- The tail stock is as rigid as a wet noodle. It would probably suffice for tail support, and the dead center that came with it is probably functional enough. It has a short morse taper on it so the tail stock doesn't have to extend three miles out to engage it. My jacobs chuck from the wood lathe..... it's almost at full extension and the rigidity leave a lot to be desired. not even sure of the alignment, TBH. But that is something I will address once it has a permanent home and is bolted to something solid.
- The handles on the cross feed and compound feed have a habit of unscrewing themselves. Nothing some loctite or turning a new handle won't fix, but annoying. (possibly a safety thing, now that I think on it. Really don't want my hands slipping near a chuck)
- getting the chuck jaws to come together evenly when swapping is a bit fiddly. pretty sure that's user error though.
The OH FOR F'S SAKE!!!!:
- The tool post is too high. I'm using 3/8 braised carbide tools for now until I get the grinder set up and can start grinding my own HSS tooling. (Got the blanks just need to grind them.) and my first first facing pass on the 4140 stalled out and started rubbing almost half a millimeter out from center. (yes, I checked against the dead center on the tailstock and even tried the ruler trick) took it out and filed down the underside. tried again, ruler trick said it should be fine.... nope. Now, in fairness to the lathe, I don't doubt that 4140 surface hardened on me when it started rubbing and many of my trouble stem from that. So I grabbed my mic and checked how thick the bit was..... it's has the thinnest body in the kit.... balls! I didn't think to check the cutter height as compared to the body.. need to check that. Either way... this is a problem and maybe it's one of my own creation. Input is welcome. I'm planning on getting a quick change tool post so that should alleviate the pain a bit.
- There are no gradations on the main feed. It's just a black hand wheel... future project.
Suggestions needed:
- bronze/brass gib: good idea? bad idea?
- is there anything special that bronze needs for being worked? How prone to work hardening is it? Any traps to avoid while annealing? my experience working with bronze mainly involves a carbide burr on a die grinder or throwing it in liquid nitrogen before stuffing it in a hole.
- preferences for shim stock for shimming tools in the tool post? I have brass shim stock or am I better off buying some sacrificial feeler gauges from princess auto?
- any thoughts on lowering the toolpost? Is there a place in the carriage that I should look or am I looking at having to file down the bottom of the holder to lower tool height since it seems to be across multiple cutters? Should I be looking at retooling in 5/16 unit I replace it with a quick change post? I'm leaning to retooling, but I really don't want to. I'd rather that cash went towards the better tool post.