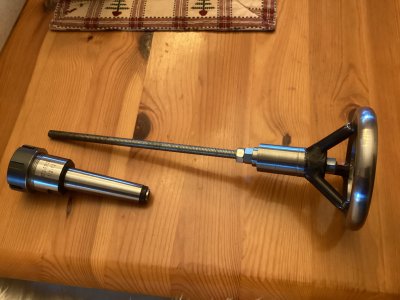
Only challenge is stock can't pass through the chuck.This is a SUPER easy option for him.

Only challenge is stock can't pass through the chuck.This is a SUPER easy option for him.
Yes it needs a 1/2-13 drawbar. Length of all-thread, a nut and large washer and job done.Doesn't the ER arbor need to be sucked in with a draw bar? Does he have a hole through the existing spindle?

The first 1/2" or so is a bit messed up but the rest felt good.David wasn’t Golems spindle MT 3 inside taper galled & generally destroyed & unusable?
I must’ve missed it. My Bad?
This is my MT3 ER 32 chuck.
When it arrived i noticed it was 1/2-12, i wasn’t paying attention, thought it was normal 1/2-13.
I made a sleeve 1/2-12 od to 3/8-16 id so i could use it with my homade , 3/8-16 draw bar.assy.
A gentleman and a scholar.I have to run to Home Depot @Golem Pens, I'll drop it off for you

The first 1/2" or so is a bit messed up but the rest felt good.
Unfortunately notDo you have a MT3 taper reamer you could lend @Golem Pens ?

Don't forget the motto on this forum is to get everyone to spend money.... ha ha...I don't mind buying one to prevent damage. Especially if someone points me to a suitable/good enough unit.
Well, my bad, that just might work then.The first 1/2" or so is a bit messed up but the rest felt good.

Provided I can source the right all thread rod, not a big issue.
A 12" length of all-thread is ... $3.38 at the Home Despot at the end of the block, I'll take the lazy route for now! https://www.homedepot.ca/product/pa...threaded-steel-rod-zinc-plated-unc/1000797593If it were me, I'd just single point thread a 1/2" bar. Or use a 1/2-13 die on the ends.
Up in #675 I commented that the existing ones looked skinny already but hard to judge by a pic & no followup. Maybe someone gave rethreading a go too?You don't need to cut all new threads. You can pick up the existing threads and cut them a wee bit deeper