• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

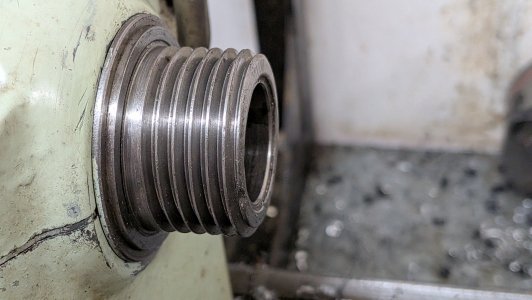
The high points across both chucks are at the same point on the spindle, so... Looking at the spindle as an issue again?

Since your spindle runout is low, I'd be looking at the chuck to spindle interface. And clean up those threads with a brass brush.
 
Yep, been in there with a brass brush already.

OK, I'd prolly try to borrow something I could verify the threads and register with then. Perhaps a known good chuck. And perhaps take your collet chuck to someone with a similar spindle and check your collet chuck on their lathe.
 
So. Not a true solution, but out of curiosity I used some brass shim at the low point of the spindle between the register and the chuck. And that's halved my runout at first blush.

Not what I want long term of course, but uh how "bad" is it to give this a go...
 
It wasn't repeatable. I took it out to make an adjustment and wasn't able to re-assemble with the same results. I likely caught it juuuuust right the first time, so I need to figure out exactly where the placement needs to be more accurately.

Good on you for realizing that. Repeatability is a key element of good metrology practices. If you can't repeat a measurement, the measurement isn't worth a pinch of racoon shit.
 
Hmm, I thought it was “a pinch of racoon shit in a wind storm”. But, distance and areas, changes sayings sometimes. LOL.
A few felt pen or pencil marks help keep track of where you were and going to.
Really, your shim adjustment did work! You learned that you can shim it to get it better, and now you know that just have to find that spot again, and then mark it. Chuck and spindle.
 
Last edited:
In post #575, the indicator tip was on the chuck body. What is the runout when on the back plate? I would check the outer edge just to the left of the chuck body, then check back side of the back plate, (only if it has been machined).
A 0.001+/- at the spindle shoulder runout will be larger farther away from the shoulder.
If there was a bit more material between the front of the shoulder and head stock, I would be tempted to take a very light facing cut off the shoulder.
There is a possibility that the collet chuck body was turned end for end when machining spindle mounting thread and then the taper and thread for collet and nut. Result, possible non parallel machining.
In picture post #500, were the bronze stock pieces with the lathe/spindle, as thought might have been to make bushings for the other spindle.

 
Back
Top