• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

Is your chuck hardened? If not, you could take a little off the nose of it, making the taper a little shorter and thus smaller diameter. Then carefully bore out your existing one as though you were just completing the whole thing. 😛
However, before doing this you want to spend a day aligning your lathe bed. No sense cutting your new taper off kilter..... if you have access to toolpost grinder, that would be even better.
That collet chuck might be hardened !
 
Michael, did you by any chance measure the runout anywhere else on the body of the collet holder while mounted on the lathe spindle? Another question, how loose are the threads on the spindle in the lathe compared to the threads on the other spindle you have? If you have a set of V blocks could you run the collet holder on to the other spindle and check the runout then with that setup. Would you be able to check the shoulder of the spindle on the lathe where the chuck and the collet holder butt up to, indicator parallel to the spindle to see if shoulder is even around the spindle?
A few thoughts, maybe an answer or 2, or a total “oh Krapp”.

 
Michael, did you by any chance measure the runout anywhere else on the body of the collet holder while mounted on the lathe spindle? Another question, how loose are the threads on the spindle in the lathe compared to the threads on the other spindle you have? If you have a set of V blocks could you run the collet holder on to the other spindle and check the runout then with that setup. Would you be able to check the shoulder of the spindle on the lathe where the chuck and the collet holder butt up to, indicator parallel to the spindle to see if shoulder is even around the spindle?
A few thoughts, maybe an answer or 2, or a total “oh Krapp”.
To add to this...... if you find your high spot if there is one on the outside of the collet chuck put a sharpie mark on the bull gear and headstock casting, then put the 3 jaw on and sweep it. Does it also have a high spot? And is it in the same place? Between chuck changes sweep both faces of the spindle register.
Also, in those pictures of the spindle nose, those little chips add up in a hurry, a dental pick and a bucket of patience goes a long way here. And, oil your threads before mounting the chucks......
 
^^^What they said.^^^
A toothbrush will get most of the chips our of the spindle/chuck threads. In post #497 the register stick out on @Model Citizen spindle is out from the headstock a lot farther than yours. When you mic the register, if it needs to be cleaned up be careful of the clearance between the chuck and the headstock that they don't interfere with each other.
 
I'll get to all these responses piecemeal as I have time, thanks all.

First, spindle runout itself in these setups is negligible, well under a thou.

I did a deeper scrub of the threads on both parts (and found a few galls I had missed in the process). That didn't make a difference in chuck runout, still seeing about 6 thou there. On both the inside taper, and the outside.
 

Attachments

  • PXL_20260106_183608161.jpg
    PXL_20260106_183608161.jpg
    1.6 MB · Views: 13
  • PXL_20260106_183850083.jpg
    PXL_20260106_183850083.jpg
    1.5 MB · Views: 14
Another thought I am having, just before tightening the chuck against the register, take another sweep of the outside of the collet chuck. I am wondering if it might be cockeyed and throwing things off. That would be easiest to repair...... I think.
 
First, spindle runout itself in these setups is negligible, well under a thou.

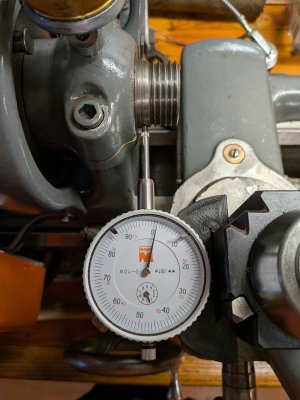
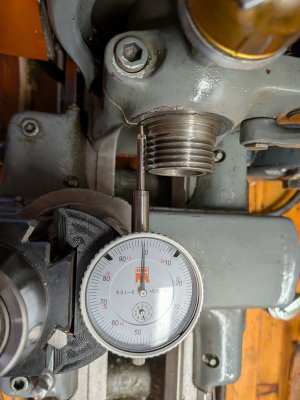
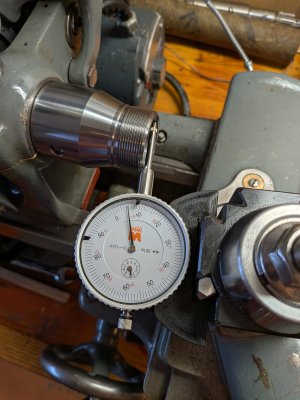
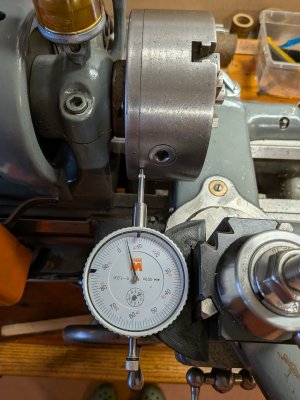
Is this "under a thou" what you show in the two photos?

I did a deeper scrub of the threads on both parts (and found a few galls I had missed in the process). That didn't make a difference in chuck runout, still seeing about 6 thou there. On both the inside taper, and the outside.

Can you show where these measurements were taken?
 
Sounds like the spindle is okay.......
Yea, which is a huge relief!

Another thought I am having, just before tightening the chuck against the register, take another sweep of the outside of the collet chuck. I am wondering if it might be cockeyed and throwing things off. That would be easiest to repair...... I think.
No noticeable difference between just snug and tight.
 
Is this "under a thou" what you show in the two photos?


Can you show where these measurements were taken?
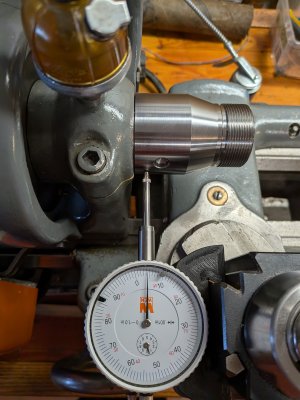
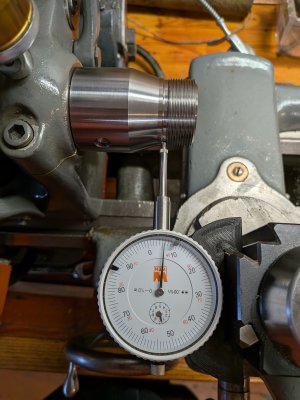
Yes, I mean not super accurate in the photos but I'm trying to show max runout.

Chuck photos.
 

Attachments

  • PXL_20260106_195444668.jpg
    PXL_20260106_195444668.jpg
    1.5 MB · Views: 3
  • PXL_20260106_195517205.jpg
    PXL_20260106_195517205.jpg
    1.7 MB · Views: 3
  • PXL_20260106_195607005.jpg
    PXL_20260106_195607005.jpg
    1.5 MB · Views: 4
So, to confirm, the runout as shown in the chuck photos above is about 6 thou?

I am with Don. I'd like to know what the 3 jaw chuck measures on the chuck diameter.
Correct.

And looks like about 5 thou (averaging for all the nicks and dings in it...)
 

Attachments

  • PXL_20260106_211535451.jpg
    PXL_20260106_211535451.jpg
    1.6 MB · Views: 3
The high points across both chucks are at the same point on the spindle, so... Looking at the spindle as an issue again?
 
If you mark the high spot (sharpie) then take it off have a tea then put it back on does the high spot stay in the same place?
If a high spot seems to be in the same location for more than one chuck then maybe the spindle is suspect.
 
No luck so far, gave it another good scrape and scrub and there's no apparent bits stuck or obviously problematic gouges (the threads are certainly somewhat beat up).

But there's gotta either be a high/point in the threads, or the threads themselves are cut a bit askew, or something...
 
Back
Top