• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

Working on my South Bend 9C

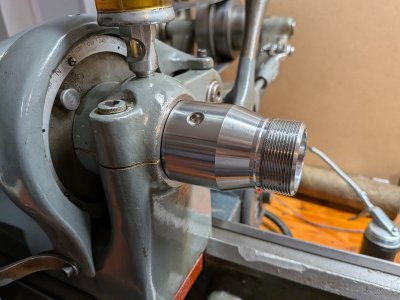
Right, so something like this (I know there are sources/ways to fabricate it, just for illustration) where you register the chuck to the faceplate for concentricity and facing? https://bmpartstech.com/product/logan-er32-chuck-collets-with-1-1-2-8-adapter-for-9-10-lathes/

@Susquatch as for workflow improvements I may spool that into a separate thread. The lack of material strength makes it tricky to do both sides without support I think.
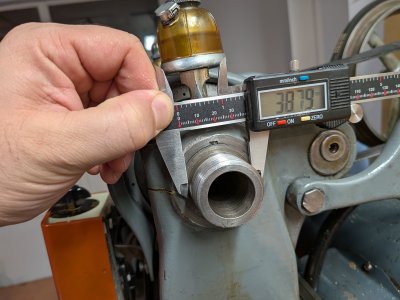
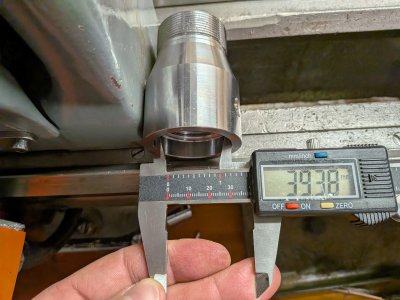
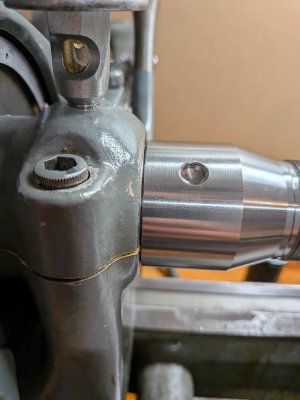
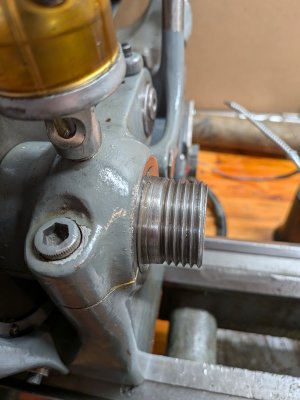
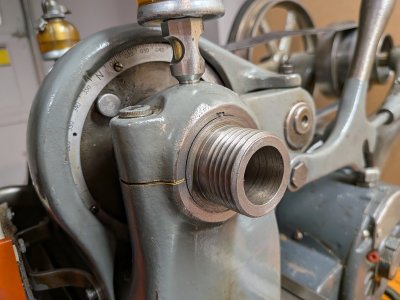
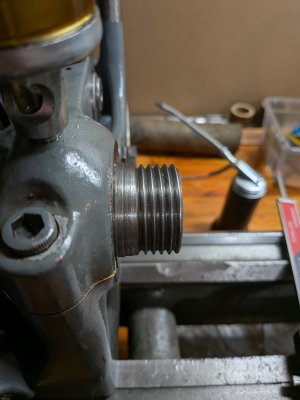
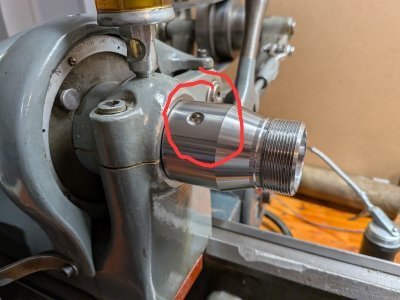
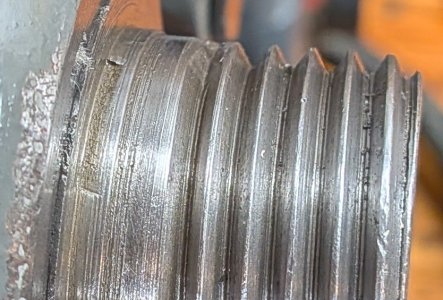
On your spindle right next to the headstock casting after the threads is a short unthreaded section. This is the register..... your chuck wants to just go over this and come up flush with the end of the register area where it enlarges to the bearing size. Hopefully that makes some sense.....
 
On your spindle right next to the headstock casting after the threads is a short unthreaded section. This is the register..... your chuck wants to just go over this and come up flush with the end of the register area where it enlarges to the bearing size. Hopefully that makes some sense.....
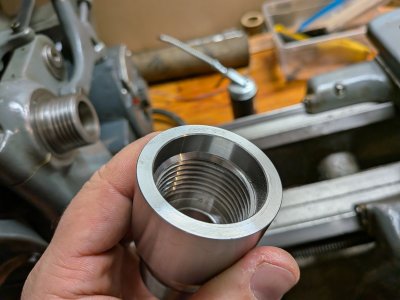
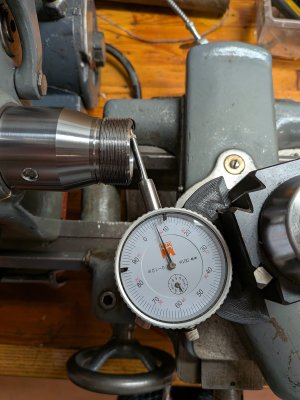
Gotcha, seems like it butts up right against the face of the spindle shoulder. About 0.6mm diameter difference between the internal/external in the register area.
 

Attachments

  • PXL_20260106_024801797.jpg
    PXL_20260106_024801797.jpg
    1.5 MB · Views: 10
  • PXL_20260106_025002241.jpg
    PXL_20260106_025002241.jpg
    2 MB · Views: 10
  • PXL_20260106_025040597.MACRO_FOCUS.jpg
    PXL_20260106_025040597.MACRO_FOCUS.jpg
    1.6 MB · Views: 11
  • PXL_20260106_024816721.jpg
    PXL_20260106_024816721.jpg
    1.5 MB · Views: 11
  • PXL_20260106_024821305.jpg
    PXL_20260106_024821305.jpg
    1.6 MB · Views: 10
  • PXL_20260106_024810655.jpg
    PXL_20260106_024810655.jpg
    1.1 MB · Views: 10
  • PXL_20260106_025020830.jpg
    PXL_20260106_025020830.jpg
    1.5 MB · Views: 10
  • PXL_20260106_025043790.jpg
    PXL_20260106_025043790.jpg
    1.5 MB · Views: 10
If lee valley sell those for wood lathes that may very well be good enough. Woodworker don't usually work in thous or tenths of mm. But they are (or have been) very good with returns.
 
Is your chuck hardened? If not, you could take a little off the nose of it, making the taper a little shorter and thus smaller diameter. Then carefully bore out your existing one as though you were just completing the whole thing. 😛
However, before doing this you want to spend a day aligning your lathe bed. No sense cutting your new taper off kilter..... if you have access to toolpost grinder, that would be even better.
 
@Golem Pens call these folks and see if they still have any of the Atlas 4-jaw chucks. They are a perfect fit and size for your lathe.

I can help you with shipping as their shipping costs when I bought a 3-jaw were pretty high.
 
Back
Top