-
Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
-
The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.
You are using an out of date browser. It may not display this or other websites correctly.
You should upgrade or use an alternative browser.
You should upgrade or use an alternative browser.
Tips/Techniques The simplest tap burner EDM I've ever seen.
- Thread starter Dan Dubeau
- Start date
Tips/Techniques
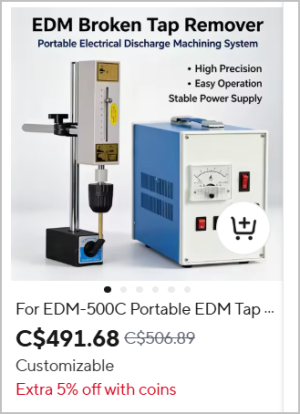
Thats cool & would certainly come in handy. Somewhere in my internet travels I read a guy bought a ready to go AliExpresss unit & it seemed to work quite well. Mostly he was harvesting the box/controls to make his own sinker for tiny small parts. He bought the graphite blocks on Ebay, made the roughing/finishing shapes & away he went. But I lost track if he did it manual peck mode or somehow integrated to veertical axis cnc.


The comments on youtube about this video are good. @kevin.decelles note. Do people use distilled water for coolant as it is less conductive? Why exactly is a pencil lead used instead of just wire?
I've reproduced a long comment from youtube by an expert below
I've reproduced a long comment from youtube by an expert below
@TheExplosiveGuy
13 days ago
I've ran EDM tap burners for ages, I've pulled out literally thousands of broken taps, drills, reamers, bolts and carbide endmills over my 20 years of being a machinist, and while your advice is solid, I can add a couple improvements to augment what you suggested;First off, the absolute best EDM burner electrode is not carbon or brass, it's pure molybdenum tubing, you'll get the longest life and fastest cut (a tube removes the least material and with the widest cross section, versus a solid rod which cuts over the entire area of it's cross section) using moly and the tube shape allows a steady flow of coolant directed right where it needs to be to flush particles up and out of a blind hole. ElectroArc sells 8" moly tubes for this exact purpose.
Second, the coolant. Coolant is extremely important for EDM work as it flushes the micro particles that get burned off and cools everything. Ideally the coolant should not be an electrolyte, you want an insulator, commercial EDM burners use a water soluble oil additive similar to machining coolant which can be purchased for relatively little money (also from ElectroArc), and a little goes a long way, a few cap fulls per gallon of water is all you need. The coolant flow rate should not be high, a light dribble is sufficient to flush and cool the workpiece and electrode, a very small aquarium pump and inline needle valve would be perfect for small jobs like this to tailor the flow rate depending on the electrode tube size. Coolant also allows higher current discharges for even faster cutting action.
Third, the electrode needs to vibrate up and down to get a fast and clean cut with mininal heat, a small spring loaded solenoid that the electrode is held in, with an interuptor switch that opens the circuit when the electrode is pulled to the top of the stroke and closes the circuit when it touches the grounded workpiece, or a square wave pulse generator would be perfect for the job, by vibrating the electrode up and down you vastly increase the number of disintegrations that can occur per second (this does require a light and constant feedrate), commercial units have a dial that adjusts the magnitude of the square wave 60Hz vibrator solenoid for selecting the right vibration strength for anywhere between .060" tubes and up to .500", the larger the tube the larger the magnitude is required (and current). The ElectroArc system I ran all those years could bore through a 1" HSS tap in about 3-5 minutes with a .500" tube, the taps were typically about 3" in length, carbide obviously takes longer at about 10 minutes at that diameter and length, but using an EDM system without vibration like shown in this video would take hours to days.
So in conclusion, you want a molybdenum tube electrode with a low flow rate of insulating coolant pumped through the inside while vibrating it up and down at varying magnitudes depending on electrode diameter to get the fastest and longest lasting cut.
Here is his power supply setup. Someone please help me (us?) understand how this works and correct my errors? He has ten 470uF capacitors in a bank wired in parallel to the power supply which charges the capacitors. Then two wires go to the EDM setup from the capacitor bank. I think then the capacitors discharge through the pencil lead and the broken tap when the circuit is completed at the work. Why does this not short out the power supply and blow the power supply fuse? Why are the capacitors even needed?
Some TIG (or MIG) welders have a pulse on/off feature - if connected up to a similar EDM setup could the welder act as the power supply?
Some TIG (or MIG) welders have a pulse on/off feature - if connected up to a similar EDM setup could the welder act as the power supply?
Attachments
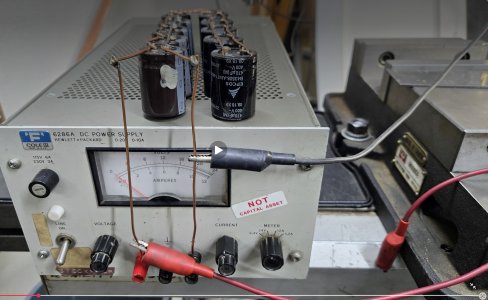
Typically power supplies like this will have both a voltage and current limit on the output. If it's a dead short, it'll just output at that specified current limit with close to 0 volts. They can also do things like charge batteries up to the voltage limit at the current limit.Why does this not short out the power supply and blow the power supply fuse?
The capacitors in this case are effectively just very low capacity, very high current output batteries and allow the high current sparking. Between sparks, the capacitors can be charged back up by the power supply.

The caps are supplying a very large amount of current in a very short amount of time. Think 12 buckets of water dumped at once vs's the house tap slowly filling them. As Sqought said the power supply likely has a protection circuit in it. Or they simply charge the caps and shut off the power supply, this would depend on how the power supply is made. Many of the designs on line have cut off circuits. Using the graphite which is conductive but will not weld to the metal being melted. The graphite has a very high melting point so the broken tap will likely go long before the graphite. Like a gouger rod but with out the air. Also the graphite will vaporize if I have that right it will not weld to the metal.Here is his power supply setup. Someone please help me (us?) understand how this works and correct my errors? He has ten 470uF capacitors in a bank wired in parallel to the power supply which charges the capacitors. Then two wires go to the EDM setup from the capacitor bank. I think then the capacitors discharge through the pencil lead and the broken tap when the circuit is completed at the work. Why does this not short out the power supply and blow the power supply fuse? Why are the capacitors even needed?
Some TIG (or MIG) welders have a pulse on/off feature - if connected up to a similar EDM setup could the welder act as the power supply?

someidiot
Well-Known Dismemberer
the power supply likely has a protection circuit in it.
It's not really "protection" as such, but an adjustable current limiter. That's an HP 6286A, which is variable 0-20V/0-10A - an older version of my bench supply (6024A, 0-60V/0-10A, dual meters). So you set the current limit - which in this case really only affects how fast the caps recharge after a burn cycle - and let 'er rip.

1018Machine
Ultra Member
Way cool Dan!