
Tobho Mott
Ultra Member
Big day here yesterday, filling a bunch of molds for 1/8 scale steam locomotive parts half full of bronze and iron. 🙁
A friend and fellow iron caster gave up for the season and drove his molds 2 hours to pour here. I started the furnace 45 minutes before his ETA knowing that melting cast iron goes a lot easier if you take your time preheating the furnace. I figured a 16# aluminum melt would be just the ticket to get things warmed up, and I happened to have just such a mold ready to go (the new crossbars worked great). I let the furnace cook for a while empty before putting in the #16 crucible full of smashed up attempt #1.
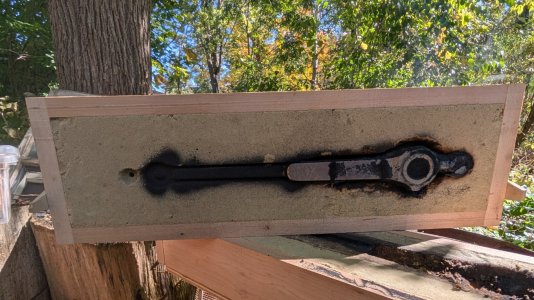
Wound up pouring the matchplate mold a few minutes after Doug arrived.
Once we got one of his crucibles charged up with bronze and into the furnace, we moved the now frozen matchplate mold out of the way and set up the first batch of molds he brought with him.
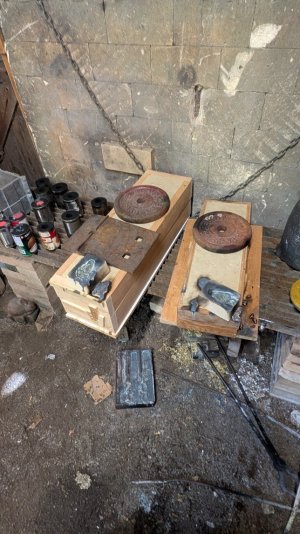
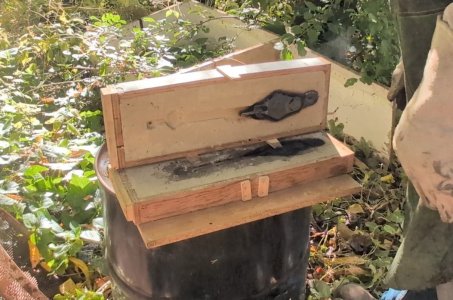
It's disheartening when they don't fill, but it's hard to guarantee success when I don't have a hand in gating the molds The metal seemed plenty hot, I guess some days you just can't win.
Then the cast iron. My A12's.last run, (at least at its original height). We also did another pour or two using another one of Doug's crucibles.
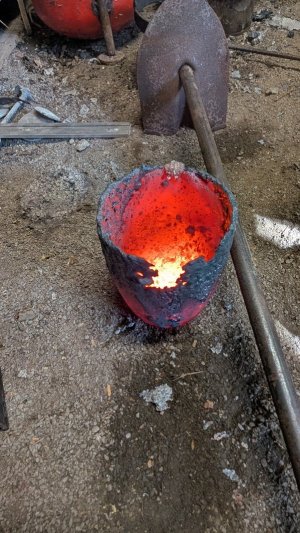
Some.important choo-choo parts I don't know the names of that had some really interesting cores (baked linseed oil bonded, old school). Very thin long sections, gated at one end.
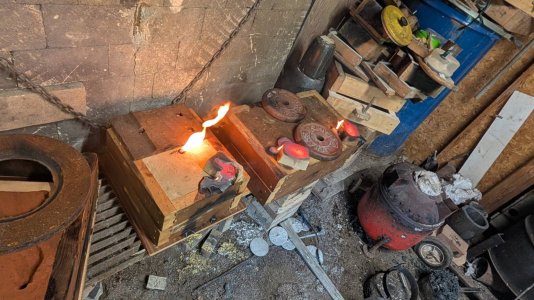
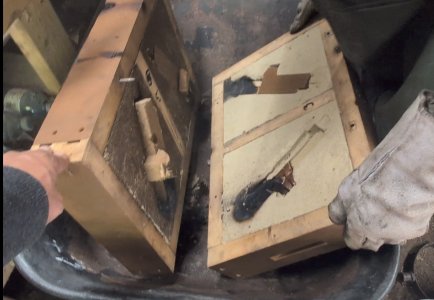
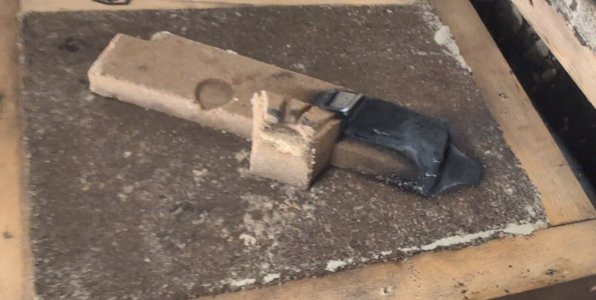
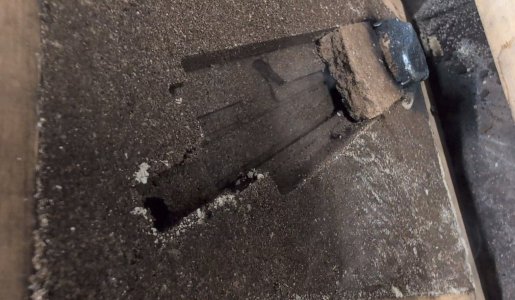
and a spoked train wheel without the spikes
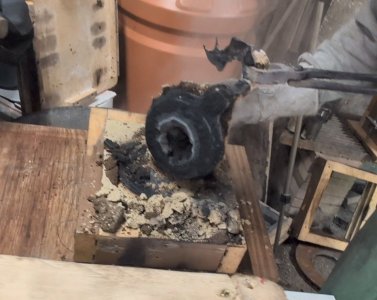
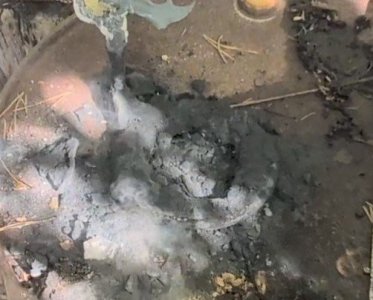
He had one more of the molds for the important part I don't know the name of, so once we knew the first mold didn't fill I did my best to open up the in gate a bit wider and cut the pouring basin a bit deeper. He uses bigger sprues and smaller pouring basins than I do, and I had difficulty keeping the sprues fill without overflowing the basins. When we opened the mold I noticed there was some loose sand in the small gate and in a few places around the mold cavity. Blew out the worst of it and tried to slick down any rough areas. Even that didn't do the trick. I think the way to get this one is to cut gates that go under the large core so it can be fed from multiple points instead of the iron having to run a long way through a thin section at one end.
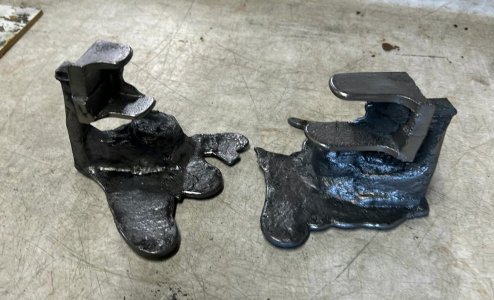
We decided to try making one more mold of one of the bronze parts from earlier. Doug started making the mold while I was dealing with the last iron pour, but once he was done the drag I offered to make the cope and try doing the gating how I thought it might work, with a runner and 3 in-gates rather than gating directly into one end off the sprue. Doug's K-Bond sand is extremely sticky compared to my well used Petrobond. So sticky that I had some trouble working with it. When I'd try to push down a loose grain so it would stay stuck to the mold, my finger would come back up with 10 more grains stuck to it and leave an even rougher spot. Tools to slick the sand down also came back up with sand stuck to them. But the mold came together not too bad in the end.
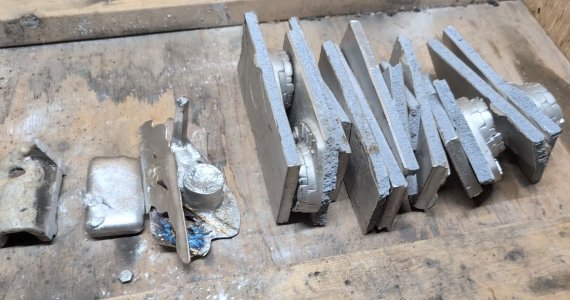
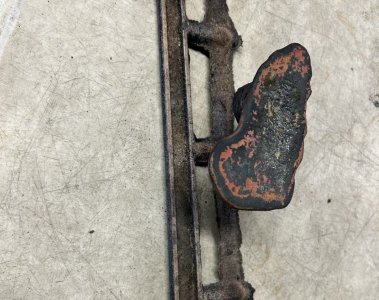
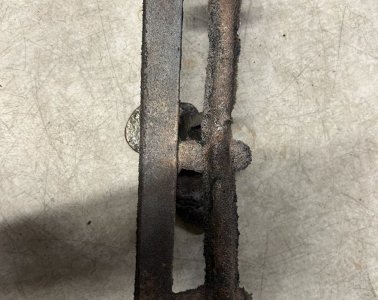
Here are the results of the first and last pours of a long day in the foundry...
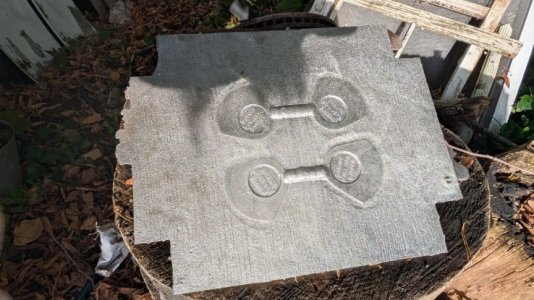
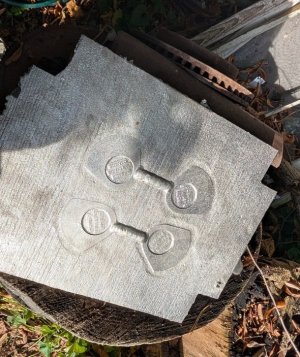
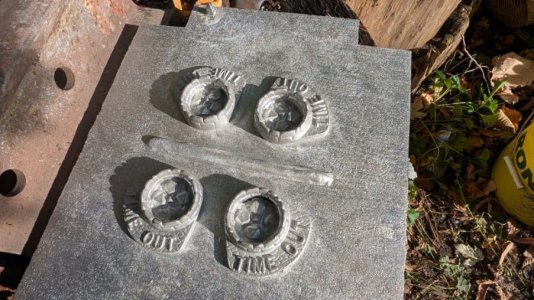
At least I don't have to mKe the giant mold a 4th time!
Jeff
A friend and fellow iron caster gave up for the season and drove his molds 2 hours to pour here. I started the furnace 45 minutes before his ETA knowing that melting cast iron goes a lot easier if you take your time preheating the furnace. I figured a 16# aluminum melt would be just the ticket to get things warmed up, and I happened to have just such a mold ready to go (the new crossbars worked great). I let the furnace cook for a while empty before putting in the #16 crucible full of smashed up attempt #1.
Wound up pouring the matchplate mold a few minutes after Doug arrived.
Once we got one of his crucibles charged up with bronze and into the furnace, we moved the now frozen matchplate mold out of the way and set up the first batch of molds he brought with him.
It's disheartening when they don't fill, but it's hard to guarantee success when I don't have a hand in gating the molds The metal seemed plenty hot, I guess some days you just can't win.
Then the cast iron. My A12's.last run, (at least at its original height). We also did another pour or two using another one of Doug's crucibles.
Some.important choo-choo parts I don't know the names of that had some really interesting cores (baked linseed oil bonded, old school). Very thin long sections, gated at one end.
and a spoked train wheel without the spikes
He had one more of the molds for the important part I don't know the name of, so once we knew the first mold didn't fill I did my best to open up the in gate a bit wider and cut the pouring basin a bit deeper. He uses bigger sprues and smaller pouring basins than I do, and I had difficulty keeping the sprues fill without overflowing the basins. When we opened the mold I noticed there was some loose sand in the small gate and in a few places around the mold cavity. Blew out the worst of it and tried to slick down any rough areas. Even that didn't do the trick. I think the way to get this one is to cut gates that go under the large core so it can be fed from multiple points instead of the iron having to run a long way through a thin section at one end.
We decided to try making one more mold of one of the bronze parts from earlier. Doug started making the mold while I was dealing with the last iron pour, but once he was done the drag I offered to make the cope and try doing the gating how I thought it might work, with a runner and 3 in-gates rather than gating directly into one end off the sprue. Doug's K-Bond sand is extremely sticky compared to my well used Petrobond. So sticky that I had some trouble working with it. When I'd try to push down a loose grain so it would stay stuck to the mold, my finger would come back up with 10 more grains stuck to it and leave an even rougher spot. Tools to slick the sand down also came back up with sand stuck to them. But the mold came together not too bad in the end.
Here are the results of the first and last pours of a long day in the foundry...
At least I don't have to mKe the giant mold a 4th time!
Jeff