• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.
  • The 2026 Calgary Area Meetup is set for Saturday May 30th at 10am. The signup thread is here! Robinhood has graciously offered to host the meetup again this year. Please note that you MUST RSVP to the notice linked above if you wish to come.

DavidR8's shop shenanigans

But the point about ensuring that if tapping 2mm or 2.5mm threads using a go/no-go test to ensure the hole is the correct size and won't break the tap.

Ya, but I'm not so sure that shoving a drill bit in there is a good gauge. But I guess you gotta use what you got.

When @PeterT mentions chuck runout, I am reminded that drill quality also REALLY matters. Especially for small holes. It is not easy to make a perfect point or a symmetric web on a 1.7mm drill. An imperfect point or an imbalanced web can lead to an oversize hole. Perhaps worse, not just a tapered hole but even one that is oversized down INSIDE the hole. Yuk!

You can only do what you can do with the tools you have. Hence my earlier comments about using a precision "sensitive" drill chuck and top notch drills. I had a Chinese sensitive drill that worked OK for what I paid for it, but I was never really happy with it. This past year, I bought an Albrecht 0 sensitive drill from @Ian Moss that is absolutely perfect! I LOVE IT! Thank you Ian!

My drills are all dormers. So I'm pretty confident that my holes are about as good as can be expected. As soon as I get the chance I'll do some tests with gauge pins. I guess we will find out then how good everything really is......
Looking forward to that.
 
Looking forward to that.

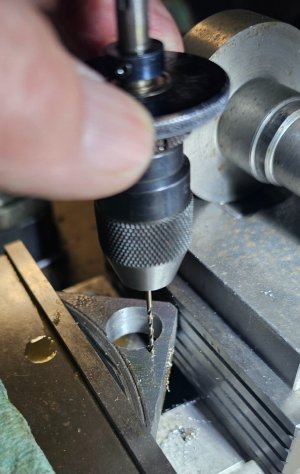
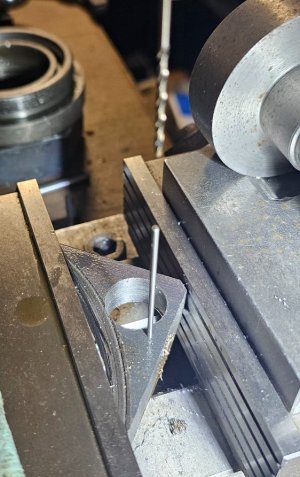
OK, using my albrecht sensitive chuck, good quality dormer drills, and grade B gauge pins, the hole enlarged by one thou for about the first 2mm of depth, and then was on size for the rest of the hole. I have no way to know if it got larger down under without sectioning and I have doubts about how well that could be measured anyway. Nonetheless, it was a nice snug fit so I have no reason to believe it happened. I doubt the extra thou would compromise the thread quality - but I didn't analyse it.

This was tested in a scrap piece of regular steel plate - nothing fancy. I used vipers venom as a cutting fluid. It entirely possible that my hand pushing down on the sensitive follower introduced a slight wobble which might have caused the slightly larger hole at the top. A sensitive drill press wouldn't have that problem.

Here are some photos:

20260321_154425.jpg

20260321_154351.jpg
 
there is a lot that could be said about drill bits and the size and roundness of the holes that they make. no matter how good the bits chucks etc., there are some important points

with or without a center punch / drilled spot the drill will start offset by some amount. it might only be a few microns, but even in the best possible case the fact that the drill has flutes means that it must start at some offset.

all drill bits are long and thin. That geometry leads to wobbles by definition.

that wobble will produce a deflection as it enters the hole that will first become worse, and then become better. As the length of the bit within the hole versus the width of the hole itself changes. This will happen because of the 'support' the bit receives from the material that it is cutting forcing the bit back into a more stable alignment with its major axis.

there will always be a critical length but I am too tired to show the math. and it isn't very important because from a practical point of view, if it matters, bore the hole or reem it. otherwise, live with it 😉
 
Looking forward to that.

Further to my earlier post. My drill stopped drilling the other day. Today I completed the hole through the half inch plate. Turns out I had simply run out of chuck travel on the sensitive shaft.

While I had time, I chased down another question I'd always wondered about. Small drill quality.

Under heavy magnification, that teeny tiny little dormer still has perfect edges and..... a PERFECT SPLIT POINT! I had always thought that split points ended at a 16th or so. Not so with Dormer. Even the smallest Dormer in my set (40 thou) has a perfectly symetrical split point under magnification. I also have some miscellaneous small drills. Some of them are dormers all of which have perfect split points all the way down to 30 thou. None of my other non-dormer bits have split points. Bonus Marks for Dormer.
 
Back
Top