• Scam Alert. Members are reminded to NOT send money to buy anything. Don't buy things remote and have it shipped - go get it yourself, pay in person, and take your equipment with you. Scammers have burned people on this forum. Urgency, secrecy, excuses, selling for friend, newish members, FUD, are RED FLAGS. A video conference call is not adequate assurance. Face to face interactions are required. Please report suspicions to the forum admins. Stay Safe - anyone can get scammed.

CX 601 Mill Belt Drive Conversion?

1763683176876.png1763683433328.png

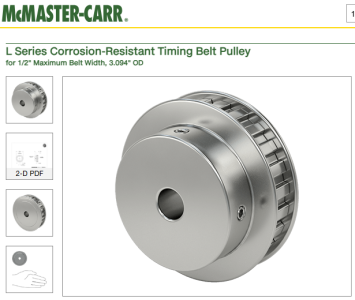
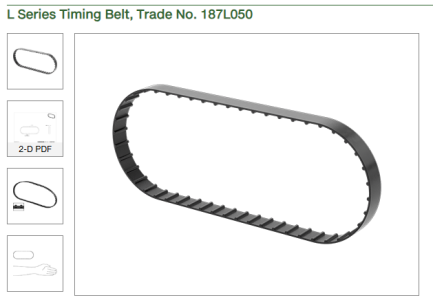
Bored out and used set screws in hub to fasten to spindle and motor shaft. Other possible part numbers are: 6495K214 and 3567N23. Can't remember exactly which ones were installed 🙁
 

Attachments

  • 1763683541156.png
    1763683541156.png
    63.1 KB · Views: 3
This has got my mind turning over how to replace my driven pulley with a smaller one to increase my spindle speed.
 
Using MS Edge it auto translates for me (if I ask it to). Chrome should offer the same thing.
Hi Gerritv,

I run Linux and primarily use "LibreWolf" browser, its based on "FireFox" only more secure. Both browsers automatically translate to English, but only the first page. It doesn't translate the second page or any subsequent ones.

However the mill head drawing for the VM32 was interesting.
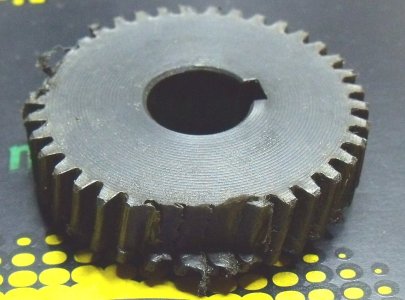
I've consider going to metal gears, however the gear i need to replace (right) would be quite the challenge to machine, its all one piece. i thought i found a steel replacement online(Left), but obviously its not going to work.

i think i want to try and stick with belt drive conversion as the gears are pretty noisy and I want to try and tweak the ratios.
Hi Gerritv, Guys,

The new gears are no more noisy than the ones on the Lathe, they do need some grease on them though. I use the lithium hub grease for the car wheels.

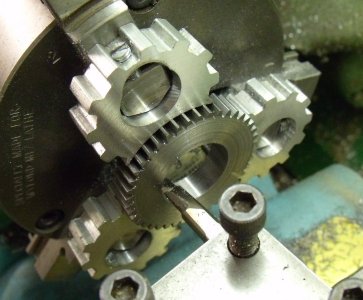
I cheated and bought five new steel gears from https://hpcgears.com/. I could have bought plastic ones but then would have still had the risk of stripping teeth. In any case the plastic gears were very little cheaper.

Gear-01.JPG

This is one of the gears.

Small_Gear-01.JPG

This is one of the gears being bored out to size.

I've more pictures if wanted.
 
Last edited:
I haven't been on here in a while and this is something I also wanted to do with my King Mill.

However I did see these gears which would be the quickest cheapest option to get your mill up and running:

Shafting Steel Gear For WMD16V WMD20V WMD25VL Milling Machine JYP250V JYP250VF JYP290VF JYP300VF Multifunctional Machine Tool​

And its on sale now for Black Friday 🙂

Hope this helps....
that's the exact gear i previously tried buying. they are the smaller set. likely for the XX25XX mills, CX600 ect..
if your interested in getting ill give you the set i have, its of no use to me.
 
I haven't been on here in a while and this is something I also wanted to do with my King Mill.

However I did see these gears which would be the quickest cheapest option to get your mill up and running:

Shafting Steel Gear For WMD16V WMD20V WMD25VL Milling Machine JYP250V JYP250VF JYP290VF JYP300VF Multifunctional Machine Tool​

And its on sale now for Black Friday 🙂

Hope this helps....

Those plastic gears are quite cheap, particularly in view of the amount the dealer wanted for them. Certainly cheap enough to buy several for spares.
 
HPC certainly has a great selection, however the shipping to Canada is as usual somewhat eye watering (FedEx)

That set is quite the find, I have bookmarked the store for potential use in the future.

I have used my King KC20VS (BF20 based machine) extensively since early last year, steel, aluminum etc. Up to 50mm face mill and 1" deming drill. No excessive noise from the gears (although low speed range is somewhat noisier).
No gear breaks. They are steel from the factory, King seems to provide better-than-bare-bones products.
 
Same here - the machine has been very solid so far. I was just a little weary of the plastic gears but so far they are holding up.

I did look into the mini pro belt drive conversion - when I first looked 3 years ago it was $350 US which I thought was way too steep. Today it's even worse $475 USD

Mini Pro Belt Drive Conversion Kit
 
Hi Gerritv,

The advantage for me was that I could take the old gears and speak directly with one of the engineers, who guided me through the gear selection and specification, for the replacement gears. All in all I effectively got about two hours of education from that visit.

I've since been and had a tour of the factory and the design and development departments. Designing a gear from scratch is no mean feat. But the software to create one is awesome. The hard part is actually inputting gear the specification.

I would use them again at the drop of a hat !
 
Before you guys all change your drivetrains to FULL metal gears . . .
The reason for the Polymer Gear is to protect your mill from SHOCK LOADS.
It saves your other gears and metal shafts from keyway damage.

It is always a good idea to design in a WEAK component to protect machinery.
 
Since there is zero information supplied from the users whose gears stripped we don't know the cause.
eg. Easy enough to make a mistake with a fly cutter too large DOC, or 50mm face mill at large DOC or feed rate to high, or climb milling with anything large diameter and lots of backlash. etc.
 
Hi Len, Guys,

Whilst in principle I don't disagree with Len, we are hobbyists using hobby machines. Impact and shock loading is important in many machines, particularly in cars and heavy machinery, but apart from errors in usage not particularly significant.
 
Since there is zero information supplied from the users whose gears stripped we don't know the cause.
eg. Easy enough to make a mistake with a fly cutter too large DOC, or 50mm face mill at large DOC or feed rate to high, or climb milling with anything large diameter and lots of backlash. etc.
i will admit, day one was my fault, i tried pushing a 3/4 drillbit thru steel without a pilot. second time they was using a slitting saw VERY cautiously, third time was using a 5/8" anular cutter. yes ill admit these are heavy operations, but nessesary operations, if my 1.5hp machine cant handle those whats the point?
 
Before you guys all change your drivetrains to FULL metal gears . . .
The reason for the Polymer Gear is to protect your mill from SHOCK LOADS.
It saves your other gears and metal shafts from keyway damage.

It is always a good idea to design in a WEAK component to protect machinery.
This was a big point of concern when i went to my local machine shop to see if they could make me some gears, they agree plasic was stupid and recomended a shear pin. if a machine has a designed weak point, that weak point should also be semi accesible, not buried in the center of a casting that takes an entire evening to take apart.

This is another reason why im leanign towards a belt drive instead of a gear train, the weak point should be the friction in the belt. if it slips you'll know your pushing the machine too hard yet you can still keep working.
 
i will admit, day one was my fault, i tried pushing a 3/4 drillbit thru steel without a pilot. second time they was using a slitting saw VERY cautiously, third time was using a 5/8" anular cutter. yes ill admit these are heavy operations, but nessesary operations, if my 1.5hp machine cant handle those whats the point?
Hi Guys,

It was a slitting saw that got me ! I was slitting a slice of 3/4" thick alloy plate. I was trying to do it in one pass. Even with WD40 as a lube the alloy was getting hot and grabbed the blade. I really should have tried multiple passes with a shallow cut.
 
if a machine has a designed weak point, that weak point should also be semi accesible, not buried in the center of a casting that takes an entire evening to take apart.
That is day one training at any Mechanical design engineering school..."put the weakest link, most likely to fail part in the middle of the floor and build everything around it" standard procedure!!
 
Back
Top