Cody S
Member
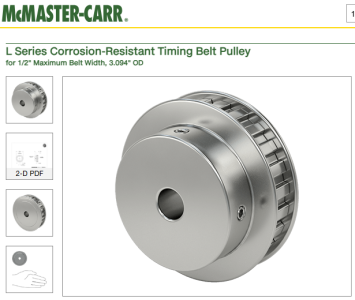
yeah that's kinda what I'm thinking, do you have a part number and source for the pulleys and belt? how did you fasten the pulley to the spindle?Here is what I did on mine:View attachment 73462

yeah that's kinda what I'm thinking, do you have a part number and source for the pulleys and belt? how did you fasten the pulley to the spindle?Here is what I did on mine:View attachment 73462

Hi Gerritv,Using MS Edge it auto translates for me (if I ask it to). Chrome should offer the same thing.
Hi Gerritv, Guys,I've consider going to metal gears, however the gear i need to replace (right) would be quite the challenge to machine, its all one piece. i thought i found a steel replacement online(Left), but obviously its not going to work.
i think i want to try and stick with belt drive conversion as the gears are pretty noisy and I want to try and tweak the ratios.
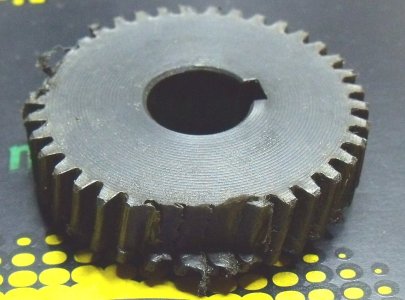
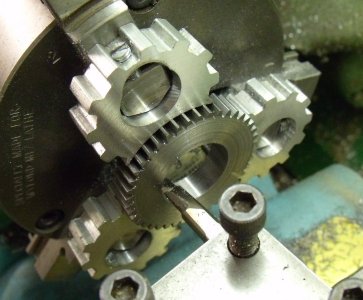
that's the exact gear i previously tried buying. they are the smaller set. likely for the XX25XX mills, CX600 ect..I haven't been on here in a while and this is something I also wanted to do with my King Mill.
However I did see these gears which would be the quickest cheapest option to get your mill up and running:
Shafting Steel Gear For WMD16V WMD20V WMD25VL Milling Machine JYP250V JYP250VF JYP290VF JYP300VF Multifunctional Machine Tool
And its on sale now for Black Friday 🙂
Hope this helps....
I haven't been on here in a while and this is something I also wanted to do with my King Mill.
However I did see these gears which would be the quickest cheapest option to get your mill up and running:
Shafting Steel Gear For WMD16V WMD20V WMD25VL Milling Machine JYP250V JYP250VF JYP290VF JYP300VF Multifunctional Machine Tool
And its on sale now for Black Friday 🙂
Hope this helps....

That set is quite the find, I have bookmarked the store for potential use in the future.

i will admit, day one was my fault, i tried pushing a 3/4 drillbit thru steel without a pilot. second time they was using a slitting saw VERY cautiously, third time was using a 5/8" anular cutter. yes ill admit these are heavy operations, but nessesary operations, if my 1.5hp machine cant handle those whats the point?Since there is zero information supplied from the users whose gears stripped we don't know the cause.
eg. Easy enough to make a mistake with a fly cutter too large DOC, or 50mm face mill at large DOC or feed rate to high, or climb milling with anything large diameter and lots of backlash. etc.
This was a big point of concern when i went to my local machine shop to see if they could make me some gears, they agree plasic was stupid and recomended a shear pin. if a machine has a designed weak point, that weak point should also be semi accesible, not buried in the center of a casting that takes an entire evening to take apart.Before you guys all change your drivetrains to FULL metal gears . . .
The reason for the Polymer Gear is to protect your mill from SHOCK LOADS.
It saves your other gears and metal shafts from keyway damage.
It is always a good idea to design in a WEAK component to protect machinery.
Hi Guys,i will admit, day one was my fault, i tried pushing a 3/4 drillbit thru steel without a pilot. second time they was using a slitting saw VERY cautiously, third time was using a 5/8" anular cutter. yes ill admit these are heavy operations, but nessesary operations, if my 1.5hp machine cant handle those whats the point?
That is day one training at any Mechanical design engineering school..."put the weakest link, most likely to fail part in the middle of the floor and build everything around it" standard procedure!!if a machine has a designed weak point, that weak point should also be semi accesible, not buried in the center of a casting that takes an entire evening to take apart.
no it doesn't, the G0704 is the CX600 equivalent, the CX601 is quite a bit largerSo does the G0704 Belt Drive Conversion Kit work with the CX601 mill?